SEMICONDUCTOR 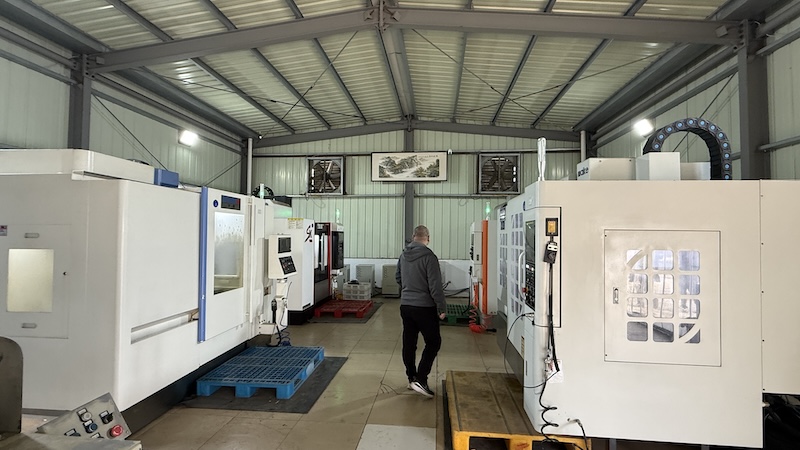
Semiconductor CNC Quartz Rings & Flanges
OD up to 650 mm · True positional tolerance ±0.01 mm · Optical Ra < 0.2 µm · Chlorine/Fluorine resistant
Get CatalogEngineered for semiconductor etch chambers, laser optics, and microfluidics. Micron-level diamond grinding, multi-axis slotting, ultrasonic drilling, and stress-relieved annealing.
Certified Precision. Audited by Global Standards.
 Onsite assessed by SGS
 Verified Supplier
 CE-marked items
Why do standard glass fabrication techniques fail in next-generation high-temperature plasma, laser cavity, and semiconductor environments? Here is what procurement engineers and search algorithms prioritize.
Fused silica and natural quartz possess exceptional hardness (Mohs 7) combined with low fracture toughness. Conventional high-speed rotary milling triggers severe sub-surface damage (SSD)—micro-fissures extending 50 to 120 microns into the structural matrix. Under corrosive chemical vapor deposition (CVD) or extreme thermal cycling up to 1100 °C, these hidden fissures propagate into catastrophic fracture.
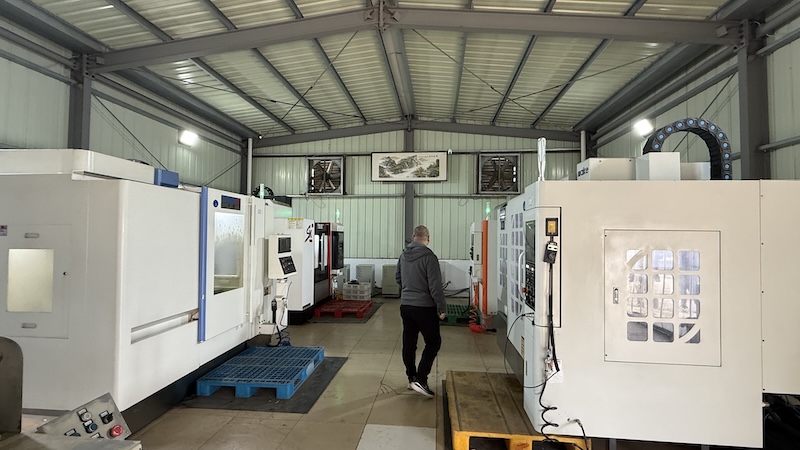
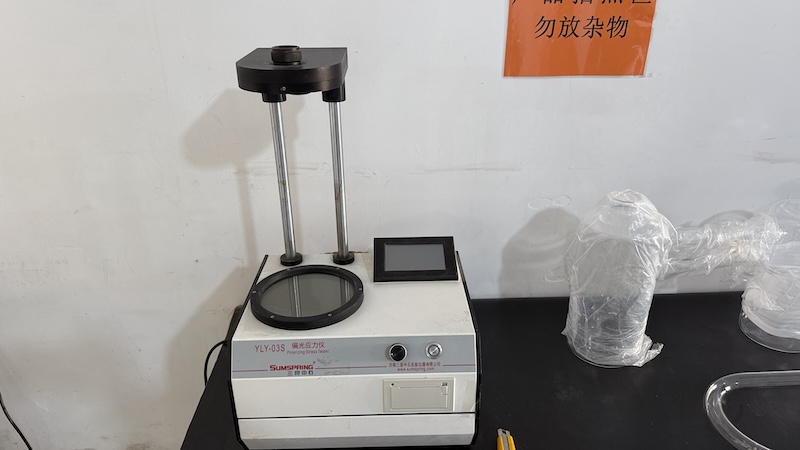
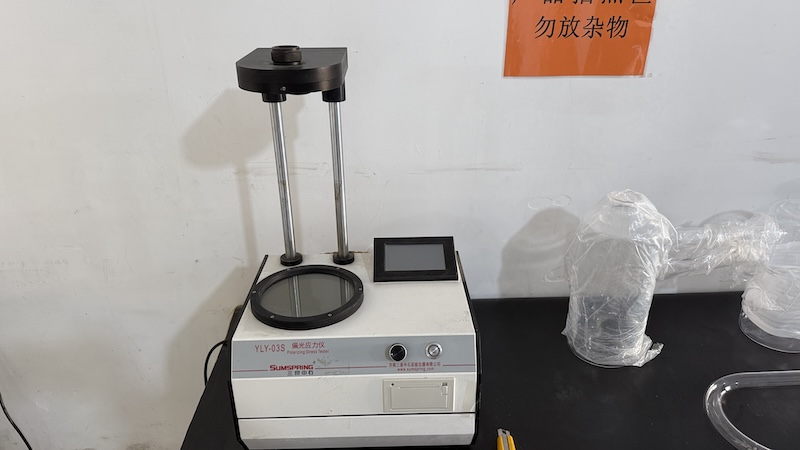
At Lovri Quartz Products Co., Ltd., we utilize multi-axis ultrasonic diamond-assisted CNC machining. High-frequency micro-vibrations continuously reduce tool cutting resistance by 40–60%, transferring brittle micro-fracture mechanisms into stable, ductile-regime machining. Every machined component undergoes thermal-gradient annealing cycles followed by non-destructive polarization stress inspection, guaranteeing zero latent micro-stresses.
A universal mistake in global procurement is specifying generic "quartz glass" without matching raw material purity with working wavelengths and plasma chemistry. Natural quartz contains trace aluminum, iron, and titanium, causing solarization under deep ultraviolet radiation. Synthetic fused silica, conversely, provides 99.999% chemical purity with negligible trace metal inclusion.
Lovri Quartz provides deep engineering guidance for selecting raw blanks prior to 3-axis, 4-axis, or 5-axis CNC machining:
Designed to strict technical specifications. Manufactured directly from your CAD, 3D STEP, DWG, or PDF blueprints with rapid validation.
OD up to 650 mm · True positional tolerance ±0.01 mm · Optical Ra < 0.2 µm · Chlorine/Fluorine resistant
Get Catalog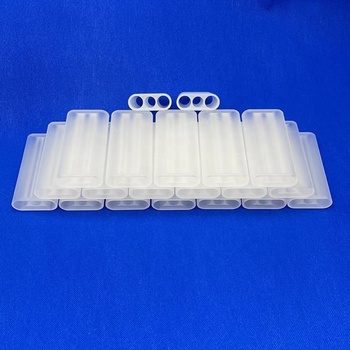
Micro-bore ID grinding · Laser cooling conduits · Tight concentricity ±0.015 mm · High thermal shock resilience
Get Catalog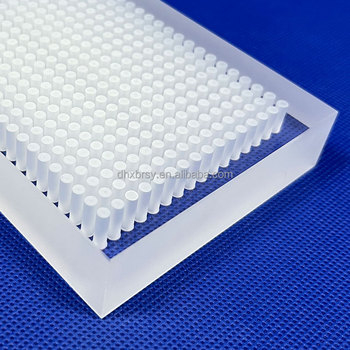
Laser & ultrasonic hole drilling · High DUV transmittance · Flatness < 10 µm · Autoclavable up to 1100 °C
Get Catalog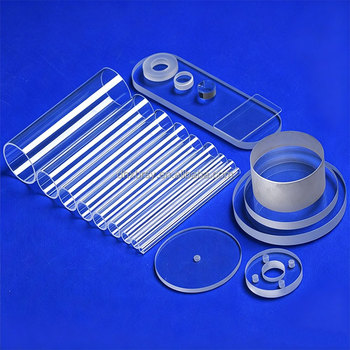
Beveled edges, mounting steps & counterbores · 20/10 Scratch-Dig · High laser damage threshold
Get Catalog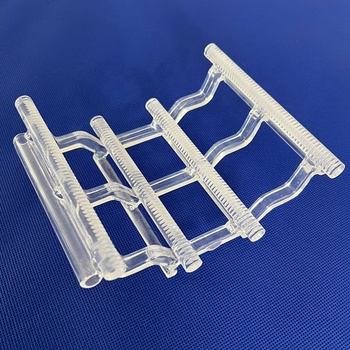
High-precision pitch slotting (±0.02 mm) · Zero warpage · 1150 °C diffusion furnace durability
Get Catalog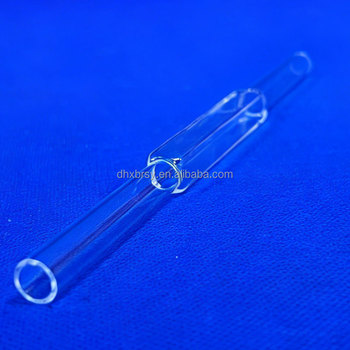
Ultrasonically machined microfluidic channels · Chemical diffusion bonding · Absolute zero dead-volume
Get Catalog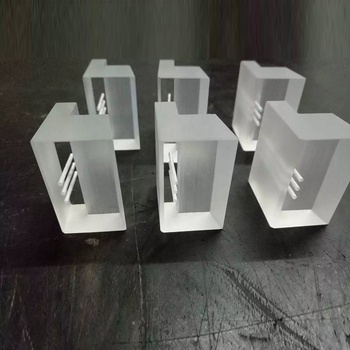
Internal and external precision threads · M-standard & custom pitches · Heat and acid hermetic connections
Get Catalog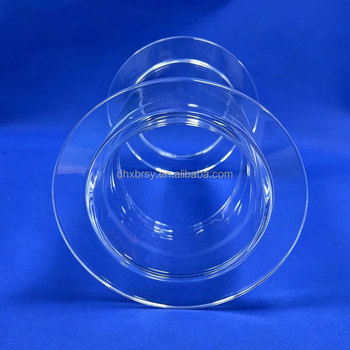
Seamless flame-fused sealing · Planar flange face milling · Vacuum tight seal for ALD/PECVD reactors
Get CatalogUnderstanding market movements enables procurement managers to de-risk supply chains and secure reliable high-volume pricing.
1. Advanced Sub-3nm Semiconductor Node Scaling: With ALD, EUV lithography, and high-density plasma etch systems operating at ultra-high RF powers, semiconductor equipment makers are replacing ceramic and alumina fixtures with ultra-pure, lower-dielectric fused silica. This demands parts with trace contamination under 0.1 ppb and geometric tolerances inside ±0.005 mm.
2. Monolithic Component Integration: Instead of multi-piece glass assemblies glued with adhesives or manually flame-welded with broad tolerances, Tier-1 OEMs demand single-piece monolithic CNC milled components. Monolithic parts eliminate outgassing risks and localized thermal expansion differentials, substantially boosting chamber MTBF (Mean Time Between Failures).
3. Shifting from Brokered Traders to Integrated Source Plants: Global disruptions have heightened geopolitical supply chain vulnerabilities. Procurement officers are consolidating vendors to certified source factories that handle raw quartz refining, automated glass drawing, and precision 5-axis CNC machining under one roof.
Combining high-frequency vibration with multi-axis indexing allows complex undercuts, micro-channels, and contoured flanges to be cut with zero edge chipping, cutting lead times by up to 40%.
Eliminating subsurface micro-fissures through controlled hydrofluoric chemical etching followed by robotic CMP yields optical clarity and surface roughness below 0.1 nm RMS.
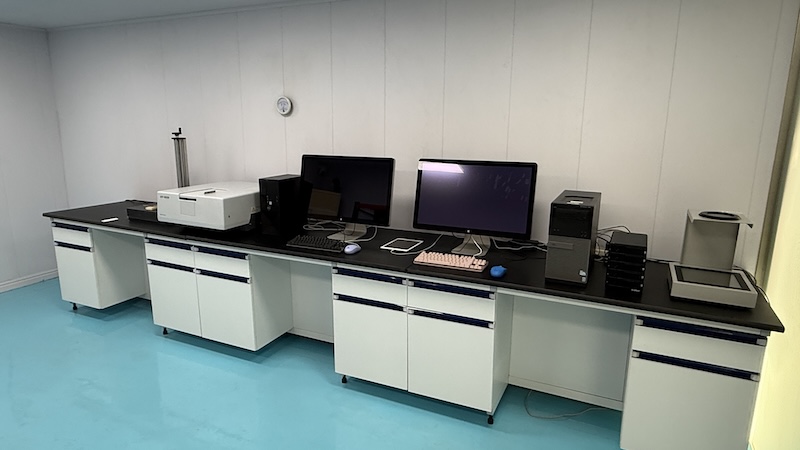
Automated circular polariscopes and laser interferometers generate quantifiable residual stress mapping reports for every custom batch before shipment.
Lovri Quartz maintains an end-to-end manufacturing route in Lianyungang, ensuring 99.99% raw material purity, strict lot traceability, and uncompromising process integrity.
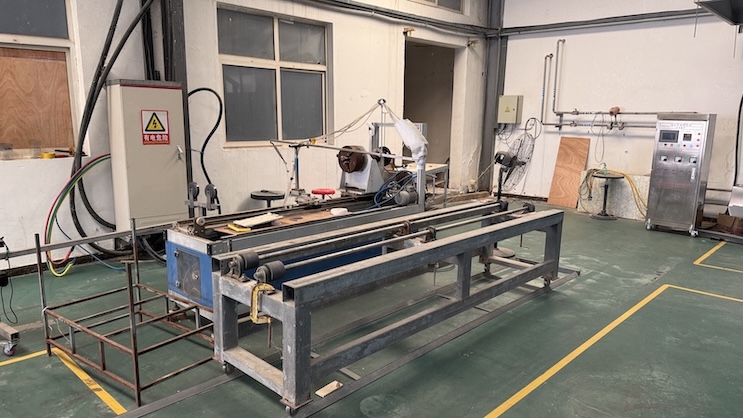
Selected high-grade natural quartz rock is sized and visually sorted.
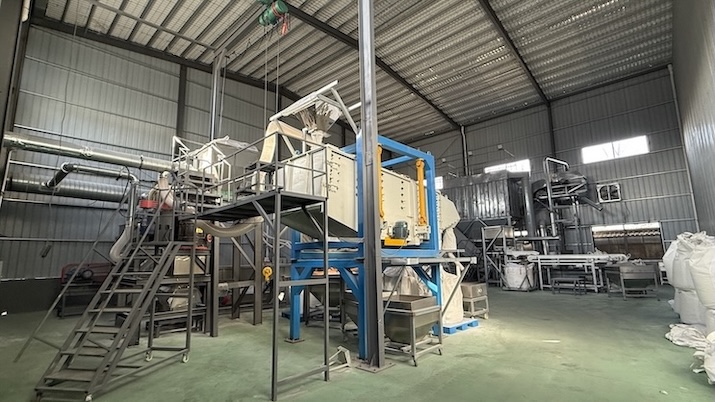
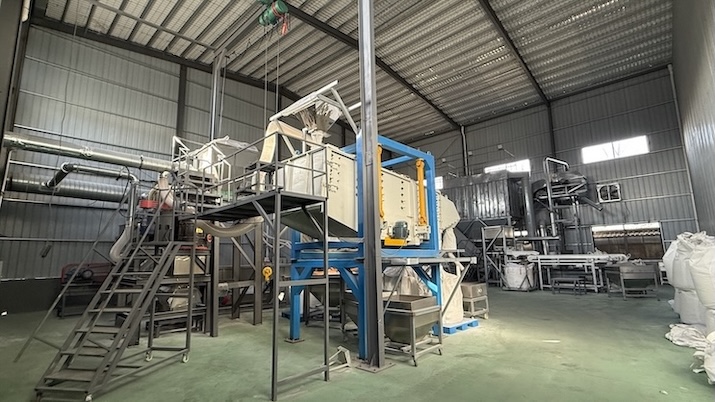
Quartz ore is pulverized into uniform high-purity silica granules.
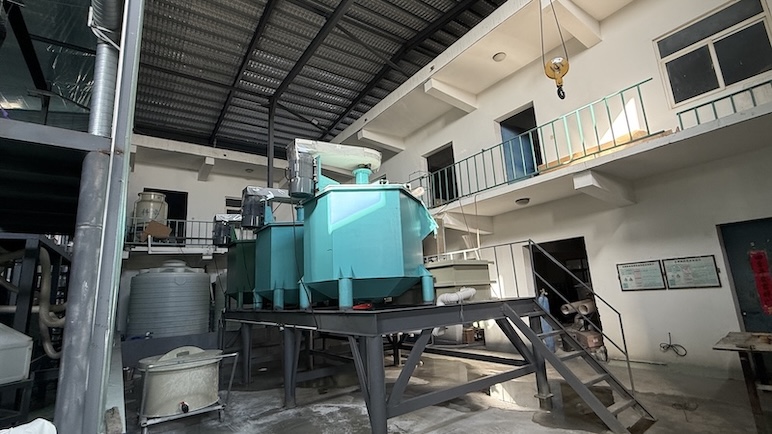
Mechanical screening separates grains to ensure precise bulk density.
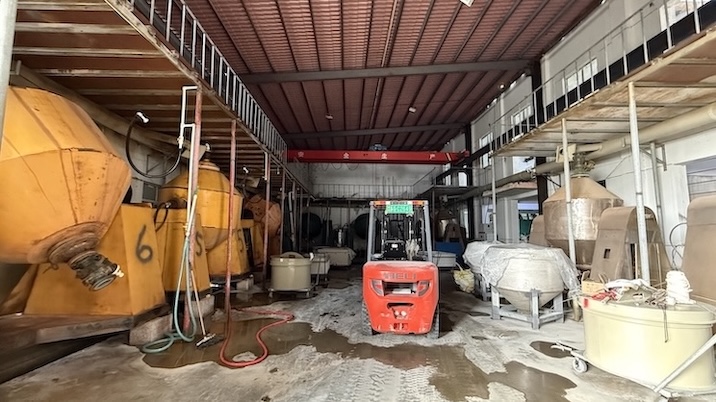
Intensive multi-stage chemical baths remove metallic ions to reach 99.99% SiO₂.
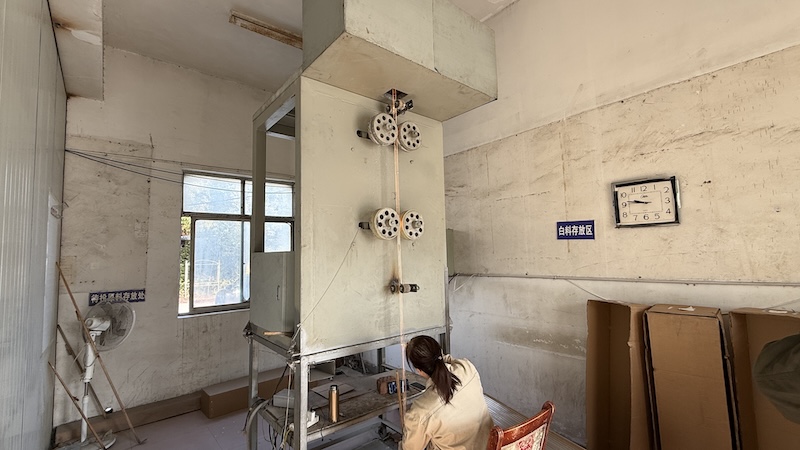
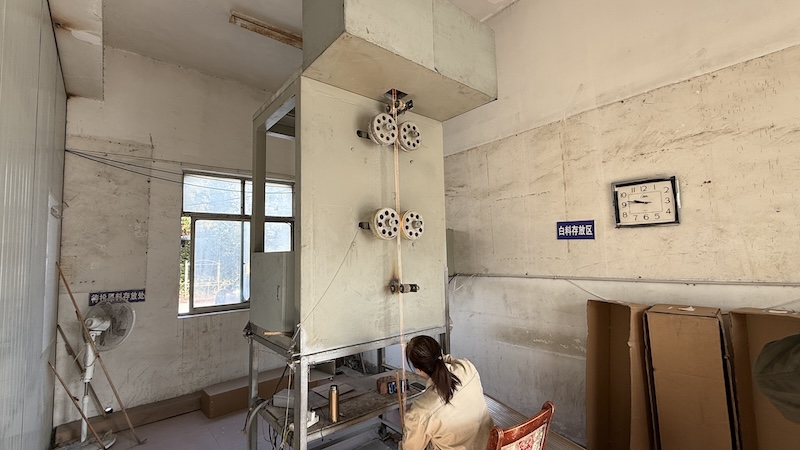
Continuous thermal drawing delivers precise raw hollow cylinders and heavy-wall rods.
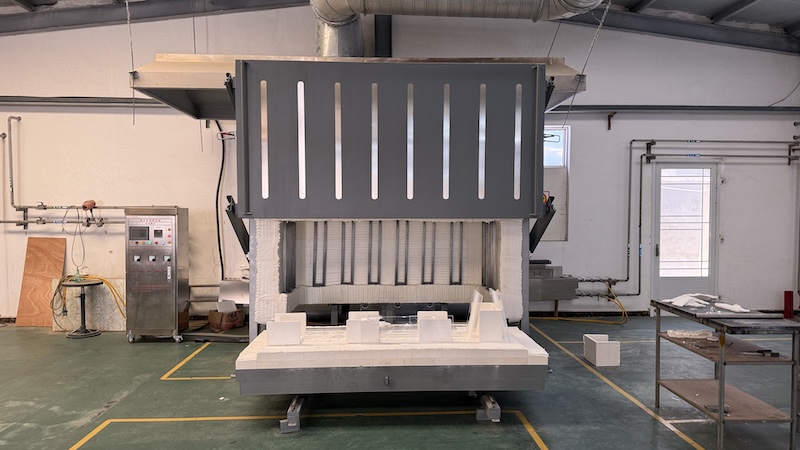
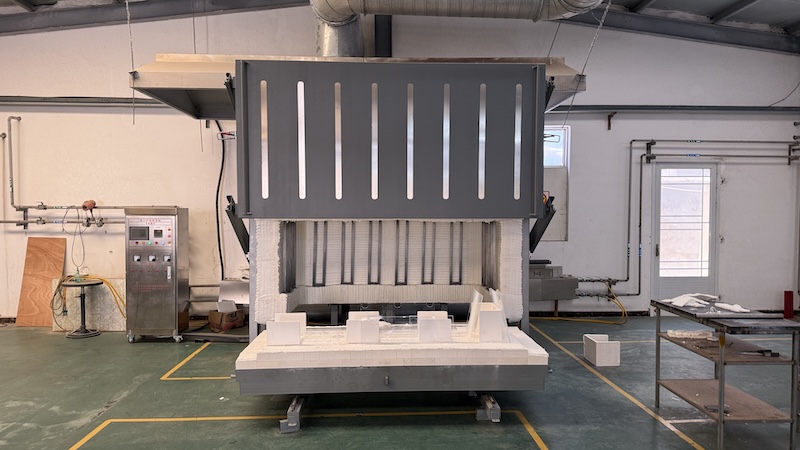
Computerized cycle annealing at 1215 °C eliminates thermal and crystal stress.
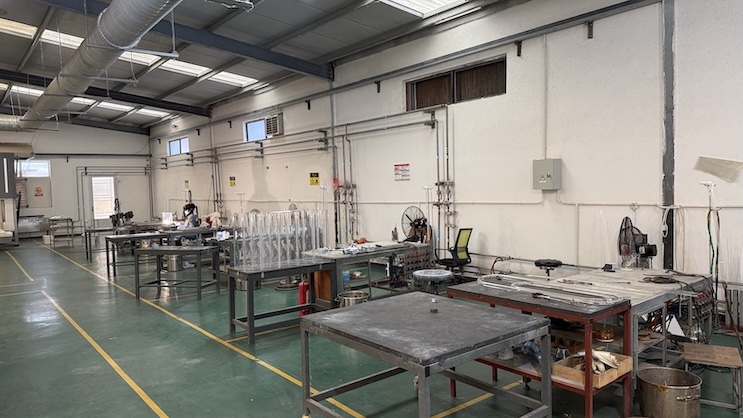
Precision hydrogen-oxygen lathes form optical domes and closed bottoms.
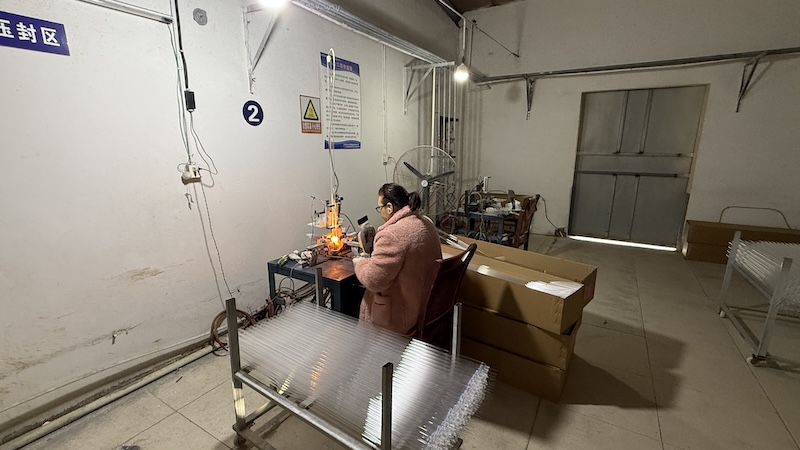
Quartz flanges, ground joints, and side-ports are fused homogeneously.
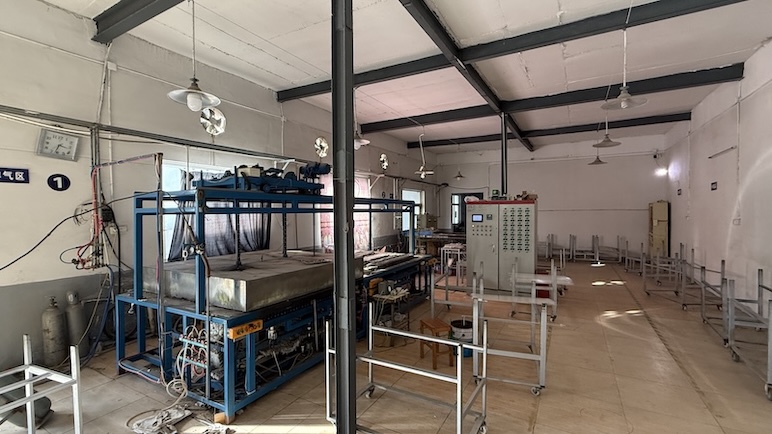
High-temperature evacuation removes atmospheric micro-bubbles.
Diamond milling, ultrasonic drilling, beveling, slotting, and profiling.
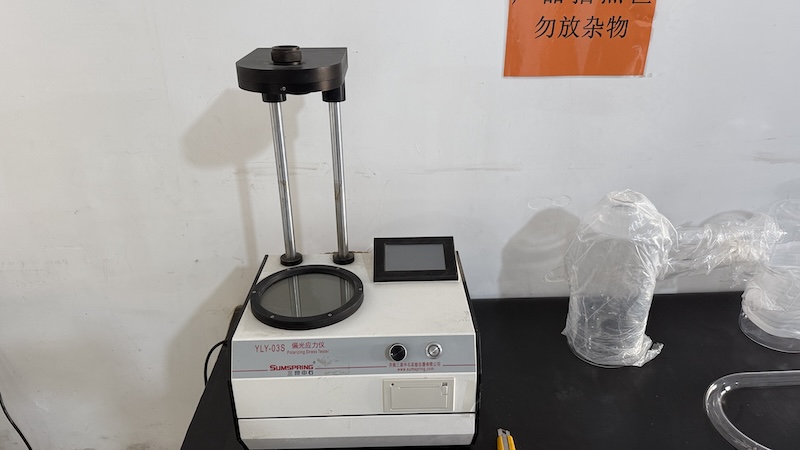
CMM dimensional metrology, optical scratch-dig checks, and polarization tests.
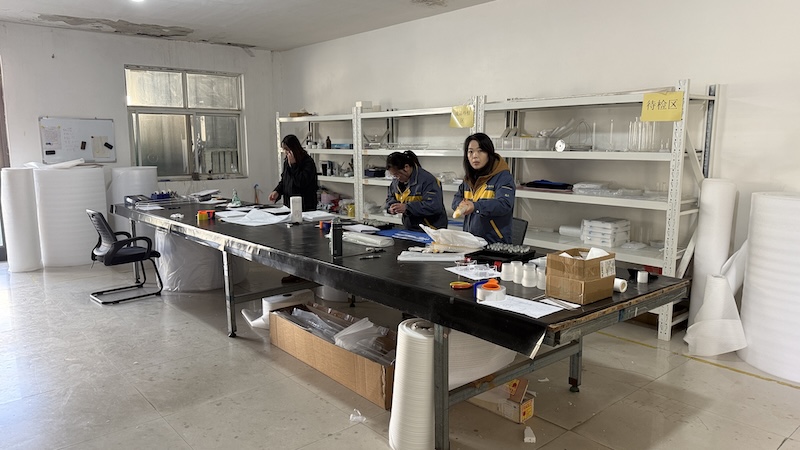
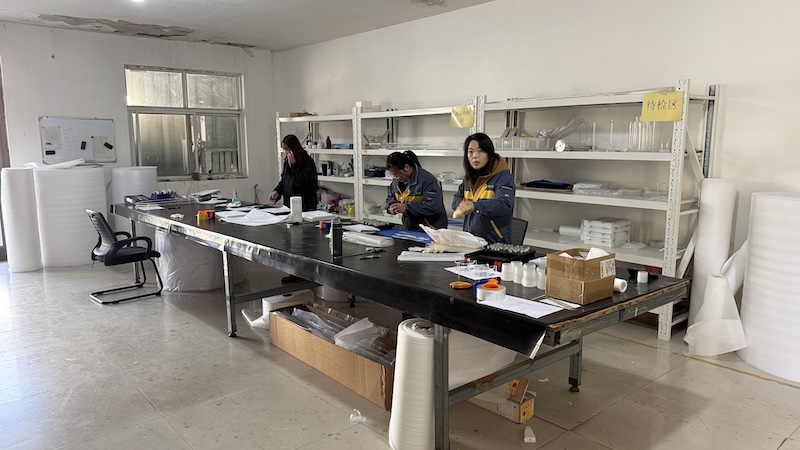
Ultrasonic cleaning, ESD vacuum wrapping, and impact-resistant foam cushioning.
Lovri Quartz Products Co., Ltd. is a vertically integrated quartz manufacturing enterprise located in the heart of Tuofeng Industrial Park, Lianyungang, Jiangsu — China’s premier high-purity fused silica industrial cluster.
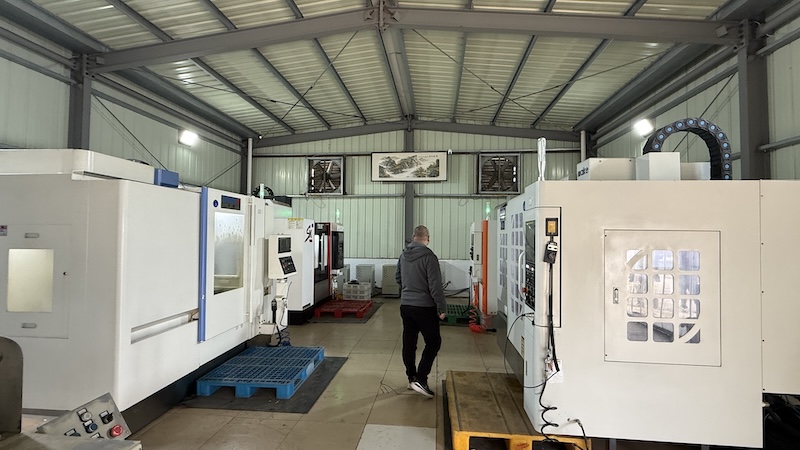
Operating across 14,271 square meters of SGS onsite-verified workshops, our specialized machining facility bridges the gap between raw material synthesis and high-precision CNC mechanical finishing. By keeping raw ore crushing, acid washing, tube drawing, thermal annealing, precision 5-axis CNC machining, and polarization testing completely in-house, we eliminate broker markups and maintain absolute control over quality and delivery timelines.
Key engineering parameters and direct answers to technical questions frequently encountered by international buyers.
| Raw Material Chemical Purity | ≥ 99.99% SiO₂ (Synthetics available ≥ 99.999%) |
|---|---|
| Machining Tolerances | Linear: ±0.005 mm | Diametrical: ±0.01 mm |
| Surface Quality (Scratch-Dig) | 60/40 Commercial | 40/20 Optical | 20/10 Laser Grade |
| Surface Roughness (Ra) | Ground: Ra 0.8–1.6 µm | Polished: Ra < 0.05 µm |
| Continuous Service Temp | 1100 °C (Short-term up to 1350 °C) |
| Coefficient of Thermal Expansion | 5.5 × 10⁻⁷ /°C (20 °C – 320 °C) |
| Dielectric Constant (1 MHz) | 3.78 (Extremely low microwave/RF dielectric loss) |
| Chemical Inertness | Zero corrosion against Aqua Regia, HCl, H₂SO₄, HNO₃ (Except HF) |
Our engineering team provides complimentary Design-for-Manufacturability (DFM) reviews within 24 hours. Send your 2D/3D technical files for immediate review.
Get CatalogSend your 2D/3D drawings (CAD, DWG, STEP, PDF) to Lovri Quartz Products Co., Ltd. Our engineering team provides detailed DFM reviews, material purity recommendations, and quotation within 24 hours.