TRIPLE-BORE 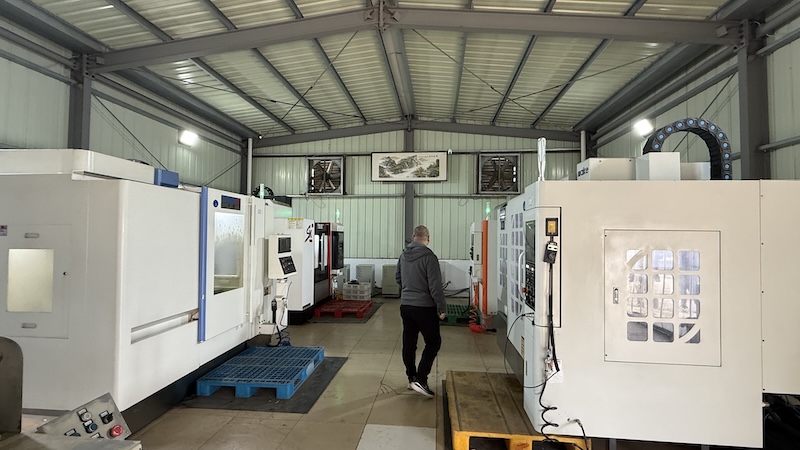
Triple-Bore Monolithic Laser Flow Tube
Accommodates 1 laser rod + 2 flashlamps in a single CNC milled body. Eliminates alignment drift; polished internal bores.
Engineered for lamp-pumped Nd:YAG, Alexandrite, Ruby, and Ho:YAG laser cavities. Featuring synthetic fused silica, cerium/samarium-doped spectral filtration, and ultra-tight multi-bore concentric tolerances down to ±0.015 mm.
Mission-Critical Optical Reliability. Certified Quality.
 SGS Onsite Assessed
 Zero-Stress Annealed
Exporting Laser Cavity Optical Sleeves Directly to Tier-1 Integrators in:
Why optical physics, thermal hydrodynamic balance, and material purity dictate the success of flashlamp-pumped solid-state laser systems.
In high-power solid-state lasers—including Nd:YAG, Ho:YAG, Er:YAG, and flashlamp-pumped alexandrite medical aesthetics systems—the Quartz Laser Flow Tube functions simultaneously as a hydrodynamic coolant jacket, an optical filter, and a physical barrier preventing electrical flashover. Operating within the laser pump chamber, these precision sleeves subject cooling fluids (typically high-resistivity deionized water or coolant mixes) across the perimeter of the gain crystal and arc discharge lamp at flow velocities exceeding 2 to 5 meters per second.
Under repetitive high-joule pulsed operation, the internal chamber temperature experiences drastic thermal gradients. Ordinary optical borosilicate or low-grade glass inevitably fractures from thermal stress shock. In contrast, high-purity fused silica (JGS1) and optical quartz (JGS2) possess an extraordinarily low coefficient of thermal expansion (approx. 5.5 × 10⁻⁷ /°C). This gives Lovri Quartz laser flow tubes the structural integrity to withstand instantaneous thermal delta shifts exceeding 1000 °C without deformation, surface micro-fissuring, or optical loss.
A key failure mode frequently queried in procurement and optical engineering platforms is the phenomenon of crystal solarization and thermal lensing caused by broadband flashlamp emissions. Xenon and krypton flashlamps emit dangerous deep ultraviolet radiation (below 380 nm). When absorbed by solid-state rods, these UV wavelengths create color centers that drastically degrade laser output power within dozens of running hours.
To eliminate this destructive mechanism without bulky optical bandpass filters, Lovri Quartz Products Co., Ltd. custom manufactures Samarium-Doped (Sm3+) Quartz Flow Tubes (available in 5% and 10% Sm2O3 formulations) alongside Cerium-doped variants. The atomic structure of samarium glass features high optical absorption across the 180–380 nm UV band and an intense absorption band centered around 1064 nm. By actively filtering 1064 nm spontaneous emission within the cavity, our flow tubes suppress Amplified Spontaneous Emission (ASE) and transverse parasitic oscillations, directly maximizing laser population inversion and boosting laser slope efficiency by up to 18%.
CNC ultrasonic micro-grinding produces surface roughness below Ra 0.2 μm, avoiding turbulence, boundary bubble cavitation, and hot-spot stagnation along laser crystals.
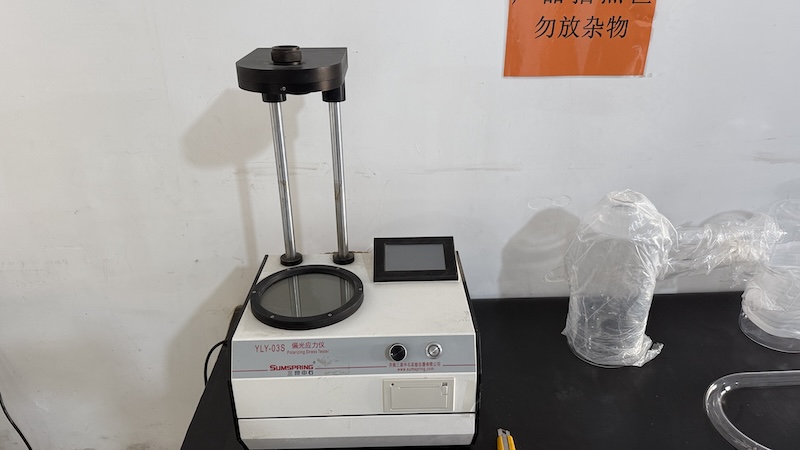
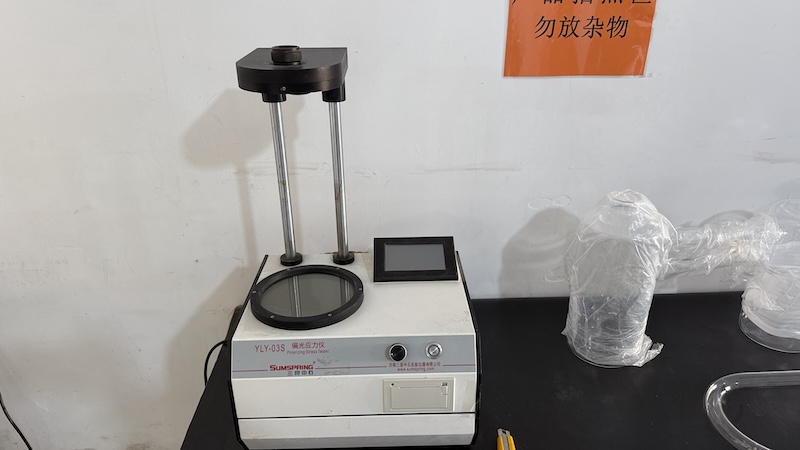
Annealing past the strain point (1120 °C) in digital atmosphere furnaces ensures optical birefringence under 5 nm/cm, eliminating thermal beam distortion and depolarization losses.
Centerline parallelism and wall-thickness runout within ±0.015 mm prevent asymmetric water jacketing, ensuring uniform radial heat extraction and stable TEM00 beam mode quality.
Select from our benchmark multi-bore, filter-doped, and monolithic pump chamber sleeves tailored for industrial, military, and aesthetic laser platforms.
Accommodates 1 laser rod + 2 flashlamps in a single CNC milled body. Eliminates alignment drift; polished internal bores.
Absorbs UV spectrum <380 nm and 1064 nm parasitic laser light. Perfect for Alexandrite & Q-Switched Nd:YAG cavities.
Integrated lamp and crystal channel with synchronized coolant flow velocity. Wall concentricity <0.02 mm.
UV transmission >90% down to 200 nm. Bubble-free optical grade fused silica for excimer and high-energy research pulses.
Cuts off harmful hard UV emissions below 380 nm, transferring pump energy into visible spectrum via internal fluorescence.
Custom bent and fused geometry engineered for compact aesthetic laser handpieces and specialized lamp packaging.
Wall thickness 0.5 mm ±0.02 mm. Maximizes thermal transfer between fluid and laser crystal while maintaining high burst pressure.
Sharp optical cutoff at 254 nm preventing ambient ozone generation in open-chassis industrial marking and cutting cavities.
Key shifts shaping procurement specifications for Tier-1 laser OEMs, research institutes, and aftermarket maintainers through 2026–2030.
Historically, pump cavities utilized individual cylindrical tubes assembled inside metal reflector shells. Contemporary design trends favor monolithic multi-bore quartz blocks where two, three, or four parallel chambers are micro-machined out of a single synthetic fused silica billet.
This eliminates the hydraulic seal leak points between disparate tubes, halves cavity assembly labor, and locks lamp-to-crystal alignment tolerances inside ±20 microns indefinitely, resisting transport vibrations and repetitive thermal shock.
As picosecond and femtosecond lasers enter aesthetic dermatology and micromachining, standard flow tubes with residual drawing stress induce phase retardation and beam ellipticity. Leading procurement departments now insist on guaranteed retardance certificates under ≤ 5 nm/cm.
Lovri Quartz Products Co., Ltd. adopts multi-step vacuum annealing combined with quantitative polarimetric computerized testing, ensuring completely isotropic refractive index profiles that preserve high beam purity (M² < 1.15).
Flow tubes exposed to mega-pulse repetitions suffer from trace mineral buildup and hydraulic micro-cavitation pitting on inner surfaces. Future procurement criteria emphasize flame-fire polished or chemical-etched inner surfaces with Ra roughness ≤ 0.1 μm.
Smoother internal bore hydraulics inhibit mineral deposits, maintain stable laminar deionized water velocity, and decrease pumping pump power requirements in portable laser handsets.
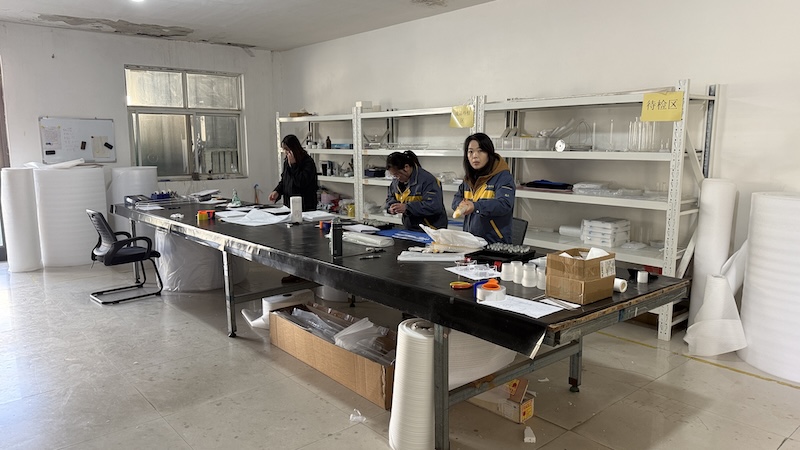
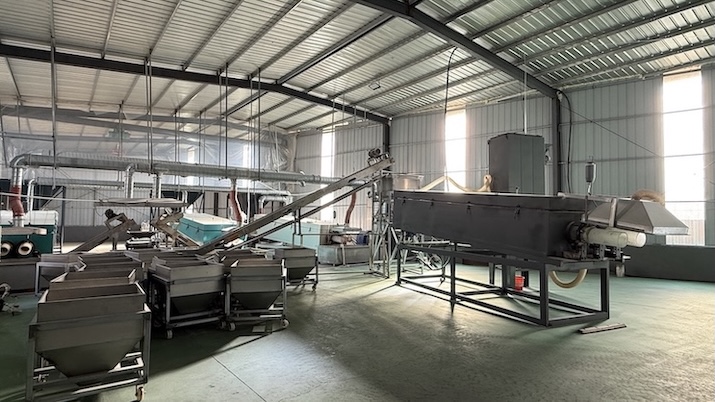
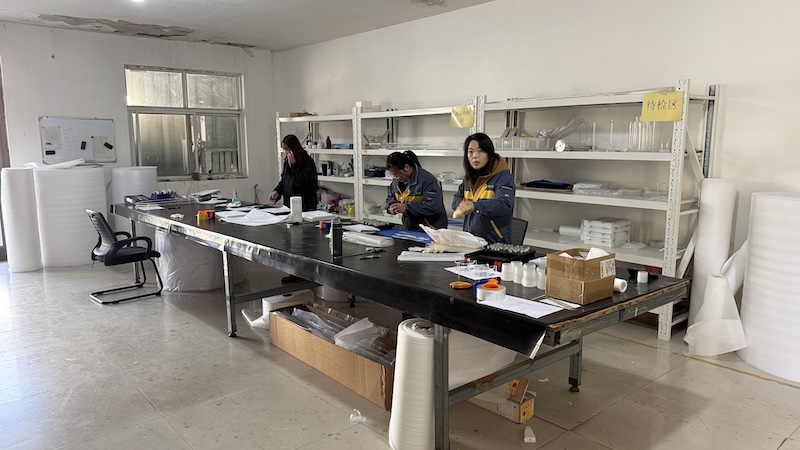
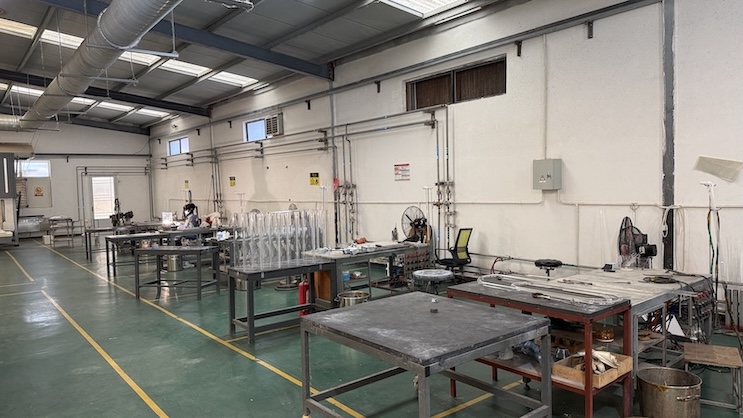
Lovri Quartz Products Co., Ltd. is situated in Lianyungang, Jiangsu, China's core high-purity silica manufacturing ecosystem. Spanning a verified 14,271 square meters, our facility integrates complete vertically integrated capabilities—from silica sand grading and electric fusing to 5-axis CNC diamond core machining, fire polishing, and optical spectroscopy.
By producing every optical laser flow tube in our own certified workshops, we ensure uncompromised chemical purity (99.99% SiO₂ minimum), total elimination of metallic bubble inclusions, and end-to-end traceability required by aerospace, defense, and medical laser system manufacturers.
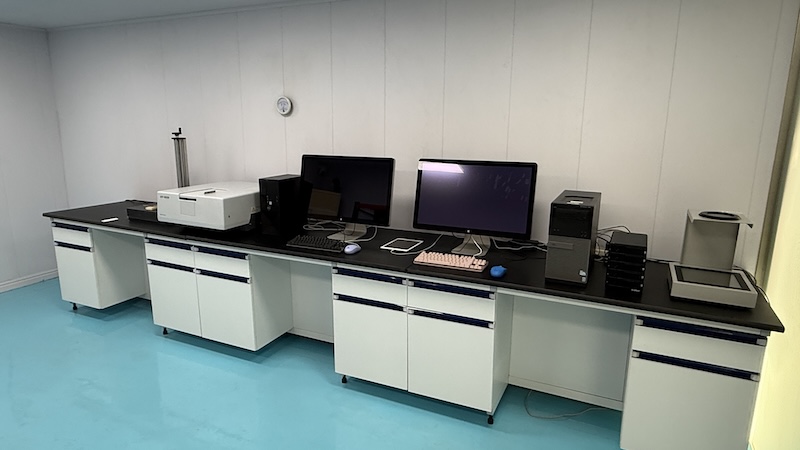
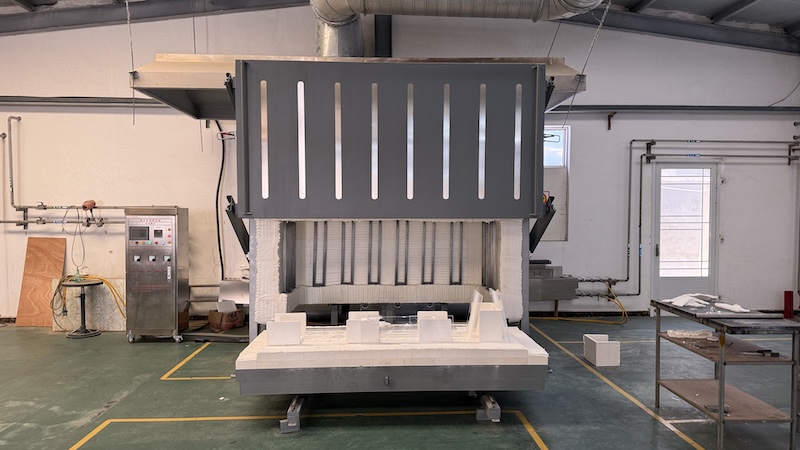
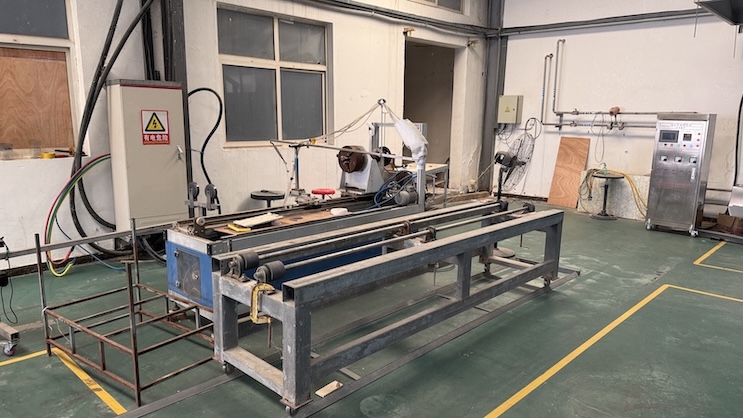
Trace every engineering step Lovri Quartz executes under one roof to deliver zero-defect laser flow tubes.
Selection of high-clarity natural crystal quartz boulders with minimal trace metal ions.
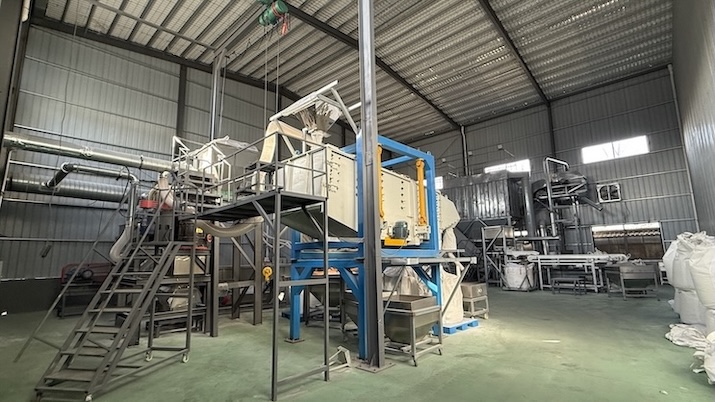
Controlled mechanical pulverization into precision mesh silica powder.
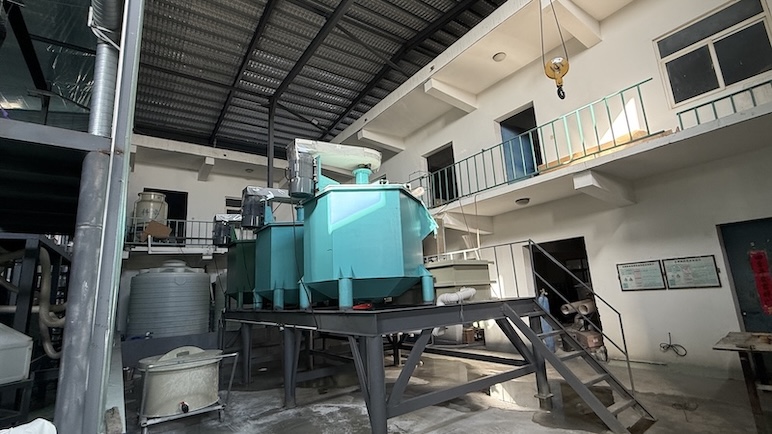
Multi-deck sieve classification ensuring uniform particle distribution and melting behavior.
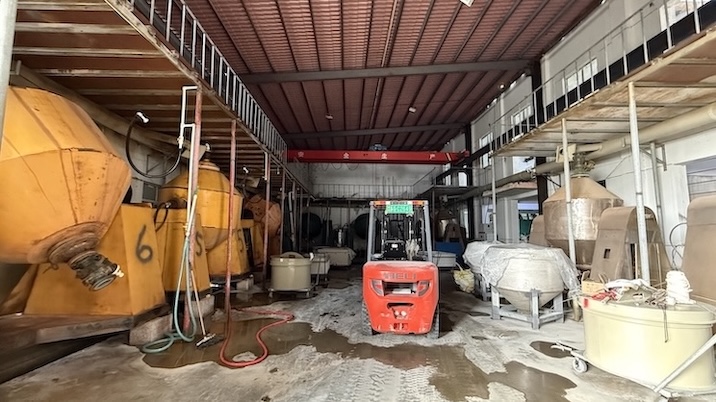
High-concentration multi-acid washing extracting Fe, Cu, and trace elements to reach 99.99% SiO₂.
Continuous thermal drawing under inert gas blankets to achieve basic laser tubing dimensions.
Programmed soak at 1215 °C to relax internal shear strain and eliminate optical distortion.
Precision oxy-hydrogen flame turning for rounded, flared, or sealed end geometries.
Seamless fusion of inlet/outlet coolant ports, manifold blocks, and mounting flanges.
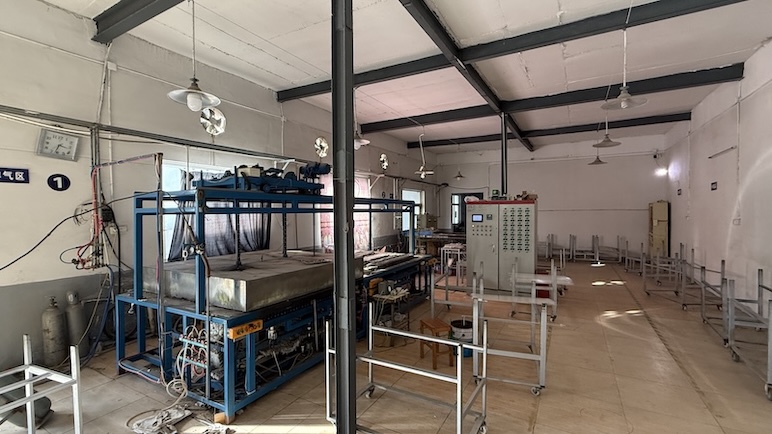
High-vacuum thermal evacuation of hydroxyl (OH⁻) groups to minimize near-IR water band attenuation.
Ultrasonic diamond core drilling and contour profiling of dual-bore and triple-bore geometries.
Polarimetric stress testing, coordinate measuring machine (CMM) runout, and spectrophotometry.
Antistatic vacuum sleeve wrapping, multi-density polyethylene cushioning, and custom crating.
Comprehensive reference parameters for optical designers, mechanical architects, and sourcing specialists.
| Property / Grade | Clear Fused Silica (JGS1) | Optical Quartz (JGS2) | Samarium Doped (Sm³⁺) |
|---|---|---|---|
| SiO₂ Purity | ≥ 99.999% (Synthetic) | ≥ 99.99% (Fused) | Silica Host + 5%-10% Sm₂O₃ |
| UV Cut-off Wavelength | ≤ 185 nm | ≤ 220 nm | Cut-off < 380 nm |
| 1064 nm Absorption | Zero / Minimal | Zero / Minimal | Strong Absorption Band (Filters ASE) |
| Thermal Expansion (20-300°C) | 5.5 × 10⁻⁷ /°C | 5.5 × 10⁻⁷ /°C | Approx. 6.0 × 10⁻⁷ /°C |
| Softening Point | 1730 °C | 1710 °C | 1650 °C |
| Fluorescence Behavior | None | None | Visible Green Shift (Harm-Free) |
| Typical System Uses | UV Lasers, Excimer, Ultra-Short Pulse | Standard Nd:YAG Coolant Sleeves | Aesthetic Alexandrite, High-Gain Nd:YAG |
| Outer Diameter (OD) Tolerance | ± 0.02 mm to ± 0.05 mm (Custom grind down to ± 0.01 mm) |
|---|---|
| Inner Diameter (ID) Tolerance | ± 0.02 mm to ± 0.04 mm |
| Wall Thickness Uniformity | ≤ 0.02 mm total indicated runout (TIR) |
| Center-to-Center Pitch (Multi-Bore) | ± 0.03 mm |
| Birefringence / Retardation | ≤ 5 nm / cm (Full polarized inspection) |
| Surface Quality (Scratch-Dig) | 40/20 or 20/10 optical grade polish available |
Certified material test reports (MTR), spectrophotometer transmission curves, and dimensional CMM reports are delivered with every volume batch.
Whether you require standard cylindrical sleeves, Samarium 10% filter tubes, or complex multi-bore CNC cavities, our technical team provides rapid drawing review, quote generation, and sample production.