Specialized Fused Quartz Series & OEM Customizations
Direct factory supply of certified optical, thermal, and custom-shaped quartz glassware built strictly to technical drawings and analytical specifications.
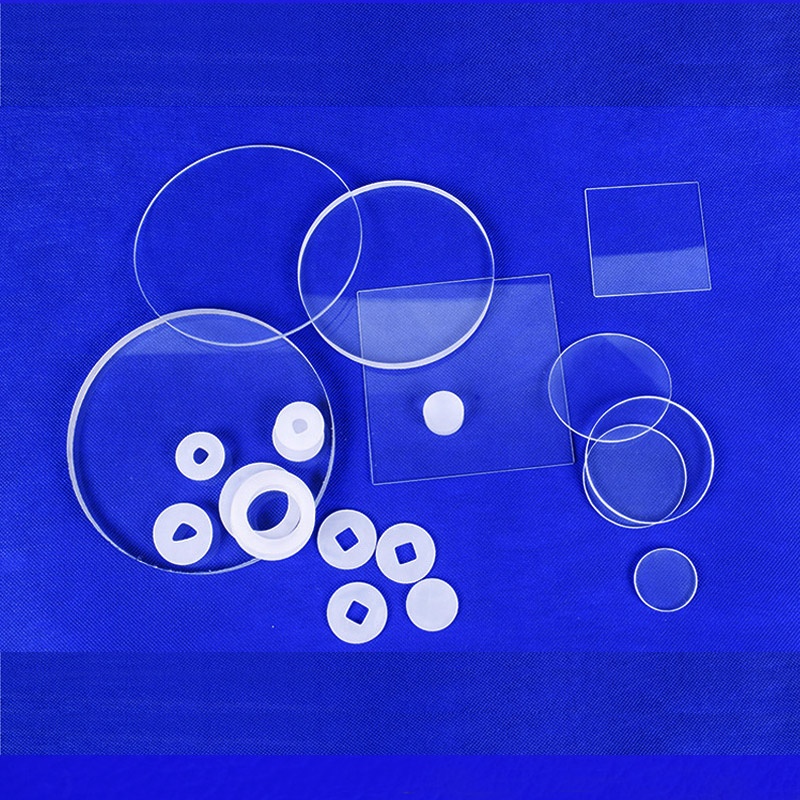
JGS1 High Purity Fused Quartz Glass Sheet
SiO2 99.99% deep-UV transparent laser plates, annealed to zero polarization stress for laser viewports and excimer optical sensors.
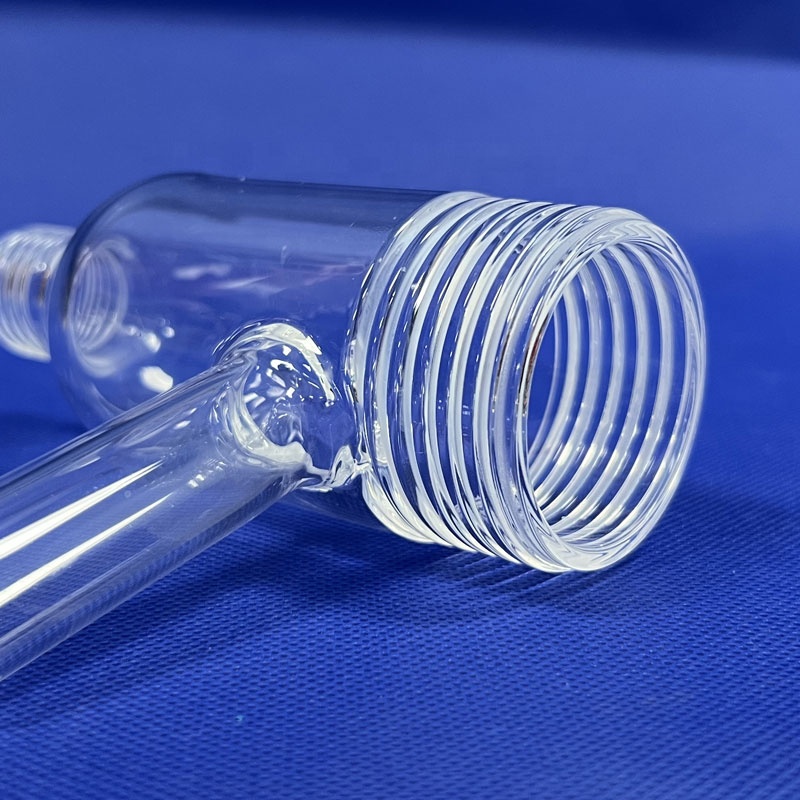
BAO RAN 515 Quartz Threaded Reaction Tube
99.99% SiO2 glass reaction vessels fitted with precision side arms and GL-threads, calibrated for continuous high-temperature catalytic flow.
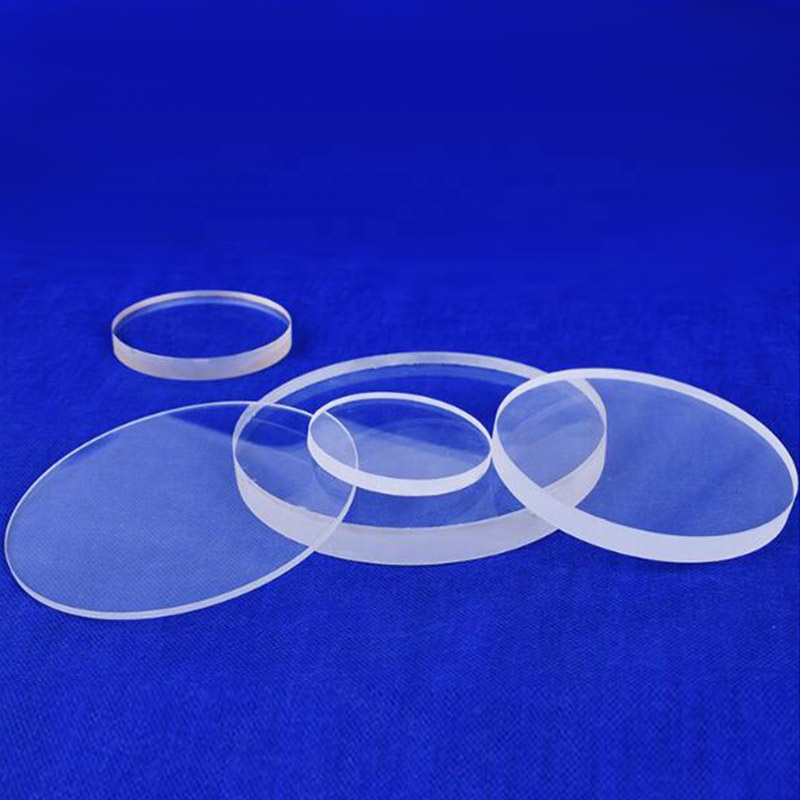
Optical Grade Polished Quartz Plate / Disc
Ultra-flat double-sided laser polished window substrates delivering exceptional transmission from 200 nm up to 2500 nm spectrums.
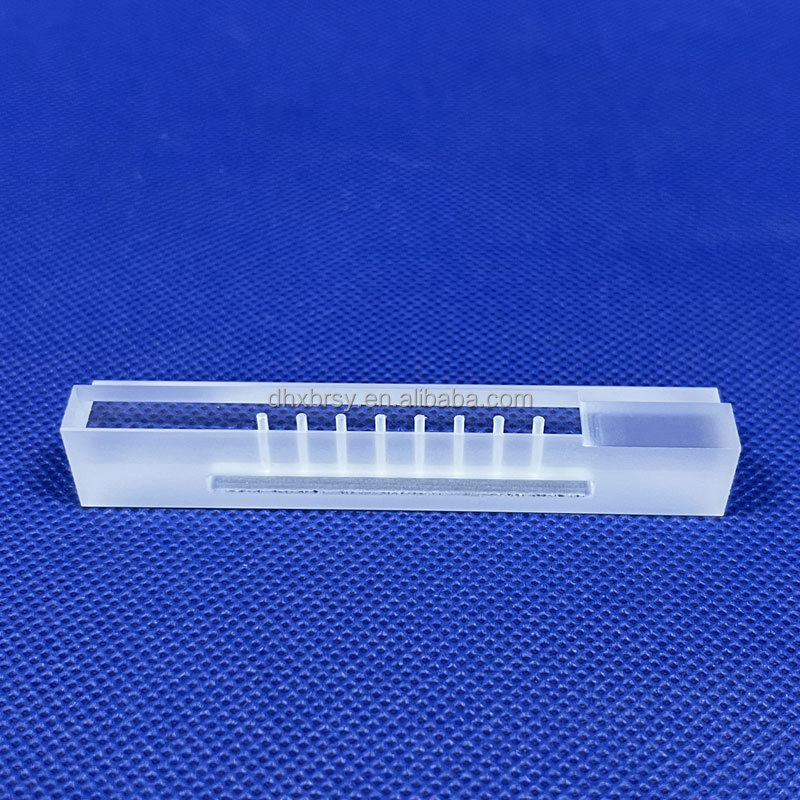
Precision Quartz V-Groove Fiber Array Holder
CNC micromachined fused quartz fixtures with sub-micron channel pitch tolerances designed for Liverpool’s photonics and optical networks.
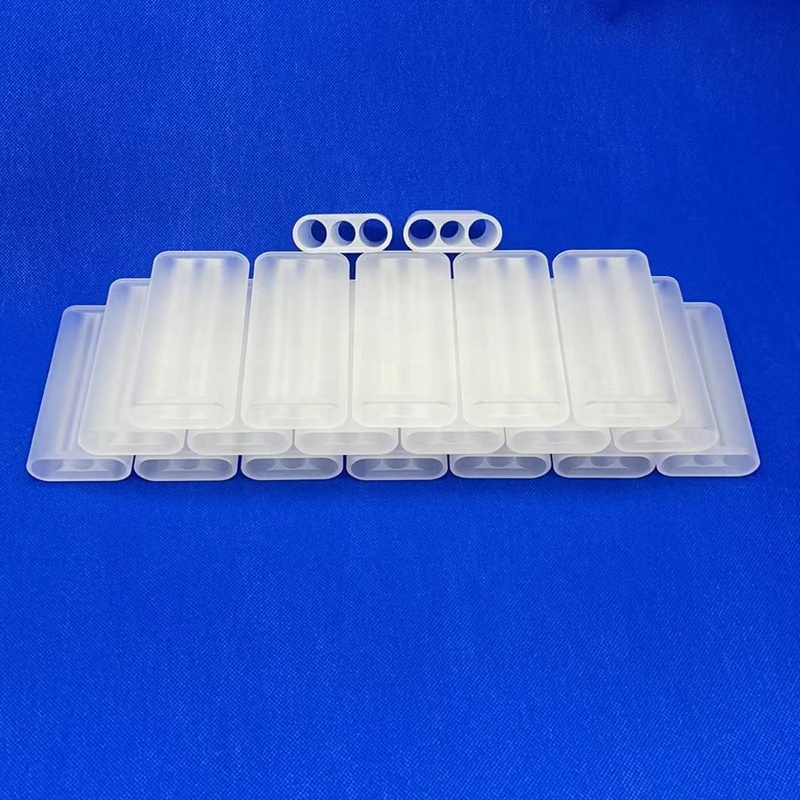
Triple Bore Laser Flow Tubes (C-Shape Bending)
Integrated multi-lumen fused silica cavity flow tubes. Fabricated through flame welding, CNC boring, and computerized vacuum forming.
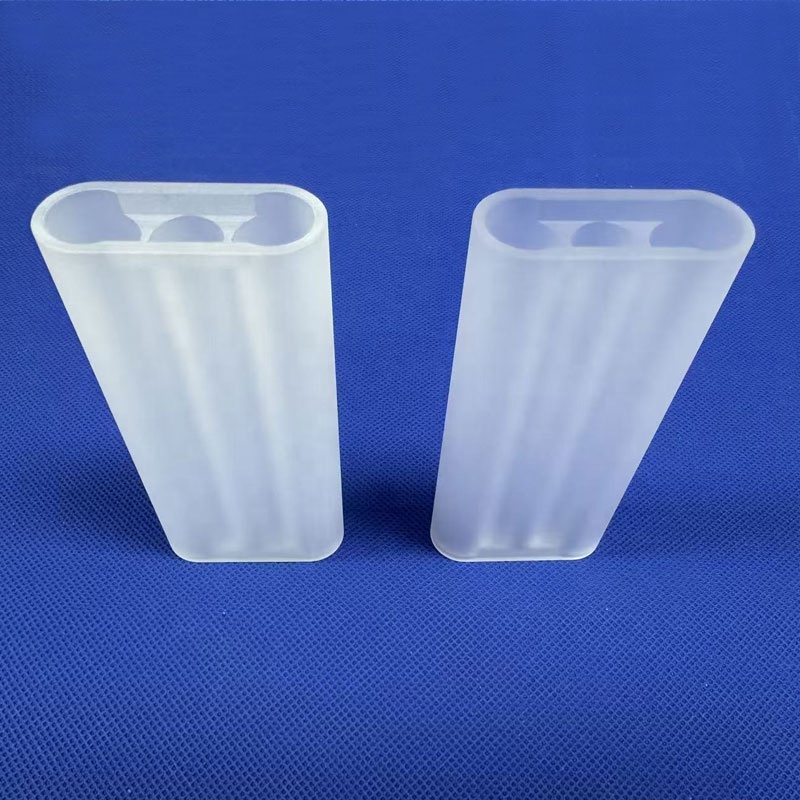
High Precision Laser Cavity Flow Tube
Engineered for aesthetic and surgical medical laser equipment, delivering high thermal dissipation and solarisation-resistant performance.
BAO RAN 419 Corrosion Resistant Quartz Sheet
Acid-resistant, white-rim chamfered double-side polished sight glass discs suited for aggressive Merseyside pilot distillation vessels.
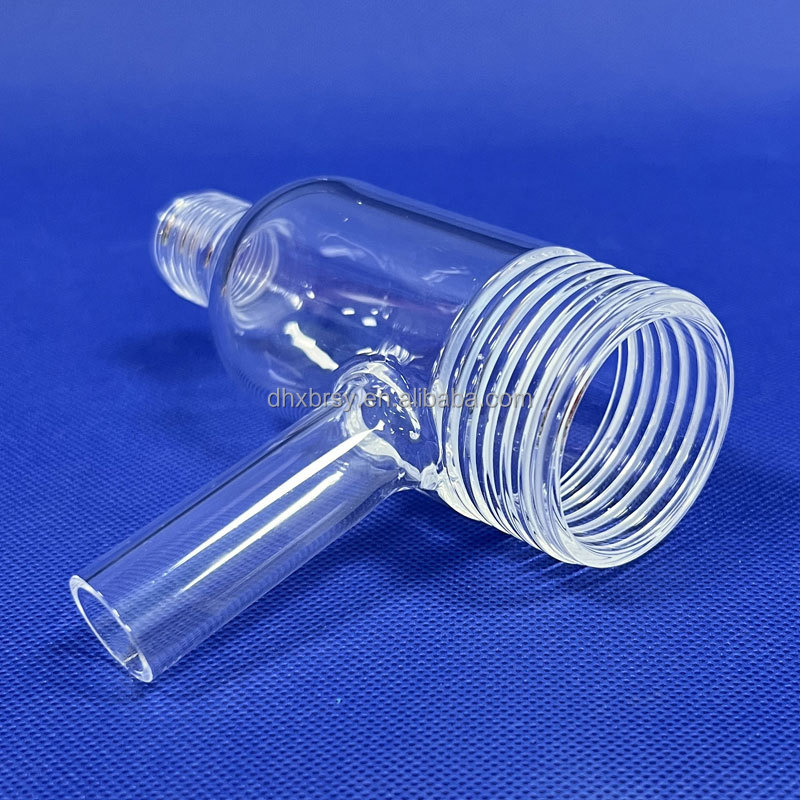
High-Temp Threaded Quartz Glass Tube
High-temperature structural tube supporting 1100°C continuous operation with CNC ground threads for vacuum furnace thermocouple sleeves.
Engineering Custom Quartz U-Tubes for Demanding Liverpool Industries
A deep exploration into material kinematics, hydrodynamics in U-bends, and high-purity thermal processing.
Custom OEM quartz U-tubes serve as the silent backbone in advanced thermal exchange, chemical synthesis, continuous UV disinfection, and photolytic scrubbing. As Liverpool and the wider North West of England accelerate investments into the Knowledge Quarter, Speke’s biopharmaceutical corridor, and low-carbon industrial hubs across the Mersey Basin, standard off-the-shelf borosilicate and lower-grade glassware are no longer sufficient. Processing corrosive media, high-intensity UV exposure, and cyclical thermal spikes exceeding 1000°C demands the crystalline-grade structural fidelity of fused silica.
When selecting a manufacturing partner for custom quartz U-tubes, engineers must balance optical clarity, wall thickness homogeneity around tight bend radii, and molecular annealing standards. A poorly formed quartz U-tube retains residual hoop stress at the apex of the curve, leading to catastrophic micro-fracturing under thermal shock or high internal vacuum pressures. As an SGS-verified fused quartz manufacturer, Lovri Quartz leverages direct mineral acid pickling, rotary induction bending, and full-spectrum polarimetric stress-relief annealing to supply Liverpool enterprises with quartz components engineered to survive extreme working environments.
Localized Industrial Applications Across Merseyside
Targeted manufacturing solutions designed specifically for regional research clusters and processing plants.
Speke Biopharma & Vaccines Corridor
In sterile biopharmaceutical processing, custom-dimensioned quartz U-tubes function as non-leaching, pyrogen-free heat exchangers and UV-C 254 nm germicidal inline flow paths. High-purity silica eliminates trace heavy metal contamination (such as Fe, Al, and Cu) common to stainless steel alloys, guaranteeing batch-to-batch consistency in recombinant protein and vaccine purification lines.
Mersey Chemical & Polymer Processing
Facilities across Runcorn, Widnes, and the Port of Liverpool frequently handle dry halogens, fuming nitric acid, and aggressive organic vapours. Our quartz U-tubes, equipped with integrated GL-threaded ends or precision ground spherical joints, serve as reflux condensers, combustion furnace tubes, and catalytic reactor loops capable of resisting acid exposure indefinitely.
Materials Science & Photonics
Liverpool Knowledge Quarter institutes require specialised optical-grade JGS1 synthetic silica U-bends for laser cooling cells, plasma generation chambers, and synchrotron beamline diagnostics. With optical transmission extending deep into the ultraviolet range down to 185 nm, our U-tubes maintain signal integrity without fluorescence interference.
Material Performance: Quartz Glass vs. Alternative Materials
Why Tier-1 engineering teams specify high-purity fused silica for safety-critical thermal loops.
| Physical / Chemical Property | Lovri Fused Quartz (SiO₂ ≥99.99%) | Borosilicate Glass 3.3 | High-Grade 316L Stainless Steel |
|---|---|---|---|
| Max Continuous Temperature | 1,100 °C (Short spikes to 1,300 °C) | 450 °C (Short spikes to 500 °C) | 800 °C (Severe oxidation above 650 °C) |
| Thermal Expansion (20–300°C) | 5.5 × 10⁻⁷ / °C (Negligible) | 33 × 10⁻⁷ / °C (Moderate) | 160 × 10⁻⁷ / °C (High stress expansion) |
| Deep-UV Transmission (254 nm) | > 90% (JGS1 / JGS2 optical grades) | < 5% (Opaque to UV-C) | 0% (Completely Opaque) |
| Corrosion Resistance to Acids | Impervious to all acids except HF & hot H₃PO₄ | Attacked by hot alkaline & concentrated acids | Susceptible to chloride pitting & acid corrosion |
| Heavy Metal Leaching Risk | Virtually Zero (< 15 ppm total impurities) | Moderate (Boron/Alumina exchange) | Substantial (Nickel, Chrome ion leeching) |
Procurement & Engineering Trends in the Liverpool Industrial Sphere
Navigating the transition toward decarbonisation, inline process analytical technologies (PAT), and direct OEM partnerships.
Decarbonisation & Hydrogen
HyNet North West and related net-zero initiatives are shifting heating away from carbon-intensive fossil burners toward electric quartz infrared heaters and high-temperature hydrogen pilot loops requiring gas-tight quartz U-tubes.
Miniaturised Flow Chemistry
Pharmaceutical and agrochemical R&D laboratories across Liverpool are replacing bulky batch vessels with continuous flow micro-reactors. Custom precision-bored quartz U-tubes enable direct in-situ photochemical reactions.
Ultraviolet Water Polishing
Municipal water upgrades along the River Mersey and industrial wastewater effluent treatment sites are mandating high-output, ozone-free or ozone-generating UV sterilisation U-sleeves capable of continuous exposure without clouding.
Streamlined Direct OEM Sourcing
Liverpool procurement teams are bypassing domestic stockists to eliminate intermediary markups and reduce engineering turnaround times. Direct factory drawings review and fast-track air shipments from Lianyungang ensure rapid delivery.
Lovri Quartz: SGS-Verified Source Factory Capabilities
Controlling the entire industrial lifecycle from raw silica crystals to specialized U-tube assemblies.
Integrated In-House Quality Assurance
Located in Lianyungang—the global nucleus of high-purity silica deposits—Lovri Quartz operates a state-of-the-art 14,271 m² production plant. Unlike downstream converters who assemble third-party tubes, we maintain sovereign control across every stage of processing.
Our U-tube forming lines utilise computer-controlled hydrogen-oxygen torches, internal gas pressure regulation to eliminate ovality at the apex, and dedicated polariscope stations to guarantee every unit leaves our plant completely strain-free.
How Custom Quartz U-Tubes Are Engineered
Precision from sand purification to final vacuum test verification.
Silica Refining
Selected natural quartz lumps are pulverized, magnetically separated, and subjected to hot acid pickling to yield 99.99% SiO₂ sand.
Continuous Drawing
Electric vacuum furnaces draw pure silica tubing with precise laser monitoring of outer diameter (OD) and wall thickness.
Rotary U-Bending
Controlled internal pressurisation during heating preserves inner bore roundness, prevents wall collapse, and forms accurate bend radii.
Annealing & Stress Test
Parts undergo 1215°C thermal annealing, polariscope birefringence testing, and foam-cushioned export packaging for shipment to Liverpool.
Frequently Asked Questions by Liverpool Engineers & Buyers
Addressing design limits, compliance protocols, and logistics into the North West UK.
What bend radii and leg spacing (center-to-center) can you achieve on quartz U-tubes?
We routinely fabricate U-tubes with tube outer diameters ranging from 3 mm micro-capillaries up to 120 mm heavy-wall industrial cooling loops. The minimum center-to-center distance depends on tube diameter and wall thickness. Typically, a centerline bend radius equal to 1.5 to 2 times the tube outer diameter can be achieved without wall thinning or cross-sectional distortion.
How do you prevent stress concentrations at the U-tube bend apex?
Severe thermal stress is naturally induced during torch-assisted bending. We subject every single formed U-tube to an automated annealing cycle in our programmable electric furnaces at 1215°C, followed by uniform controlled cooling. Each production batch is inspected via polarization stress measurement (crossed polarizers) to verify zero destructive birefringence.
Can custom connection flanges or threads be integrated into the U-tube ends?
Yes. Our in-house glassworking and CNC machining workshops allow us to weld quick-release ISO-KF / NW vacuum flanges, ground spherical ball-and-socket joints, standard ground taper joints (NS 14/23, 29/32), GL-threads with matching PTFE caps, or fused quartz flat-face disc flanges directly onto the U-tube arms according to your CAD drawing.
How are fragile quartz items protected against transit damage to Liverpool?
We employ certified export packing protocols developed over decades. Fragile U-tubes and multi-bore vessels are sealed in moisture-barrier bags, cushioned within high-density expanded polyethylene (EPE) custom shock-molds, and packed in reinforced multi-wall corrugated cartons or custom ISPM-15 export wooden crates. Full transit insurance is provided on all DAP/DDP shipments.
What documentation and material certificates accompany orders to the UK?
All shipments can be supplied with a Certificate of Conformity (CoC), raw material purity analysis reports (spectrophotometric testing confirming ≥99.99% SiO₂), polarimetric stress inspection records, and dimensional inspection sign-offs. We fully support RoHS, REACH, and custom UKCA compliance declarations on customer demand.