High-Purity Quartz Glass & Optical Tubes Portfolio
Manufactured to optical and semiconductor standards (≥99.99% SiO₂) with polarization stress relief, tight wall concentricity, and specialized geometries designed for liquid cooling and intense optical radiation.
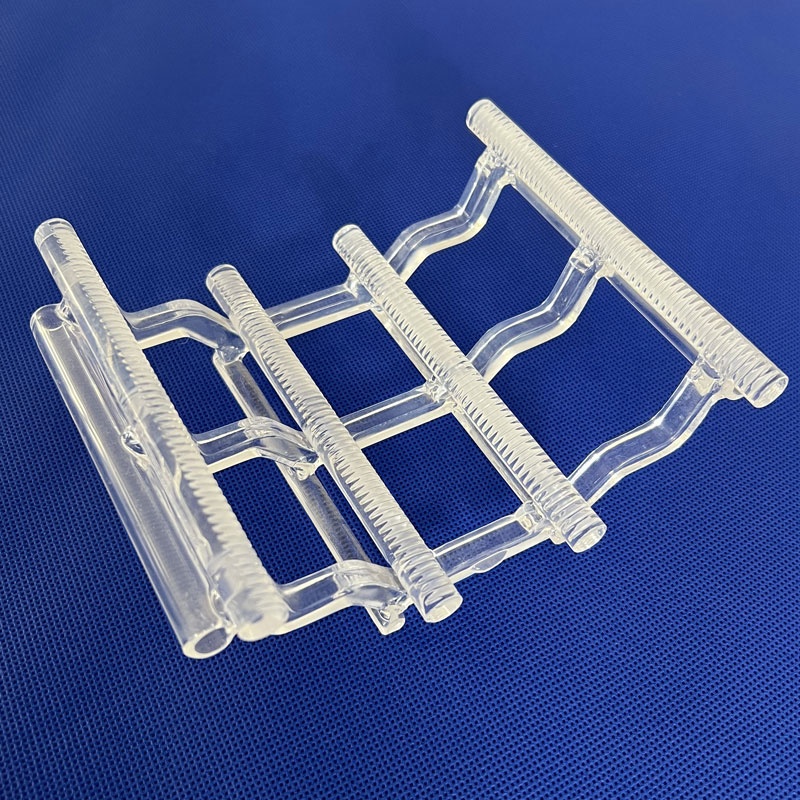
Fused Quartz Wafer Boat Carrier
Custom sized 99.99% SiO₂ carrier boat engineered for high-temperature semiconductor diffusion, oxidation, and laser annealing processes with RoHS compliance.
View Specifications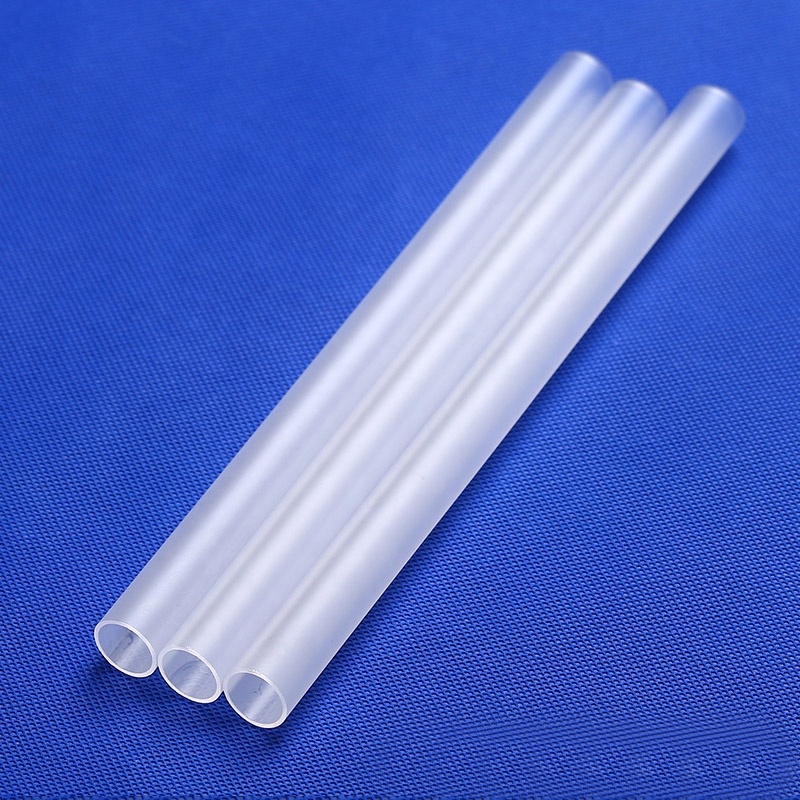
Polished High-Purity Quartz Tube
High-transmittance quartz sleeve designed for cutting, bending, and welding in industrial ozone generators, UV disinfection, and IR heater jackets.
View Specifications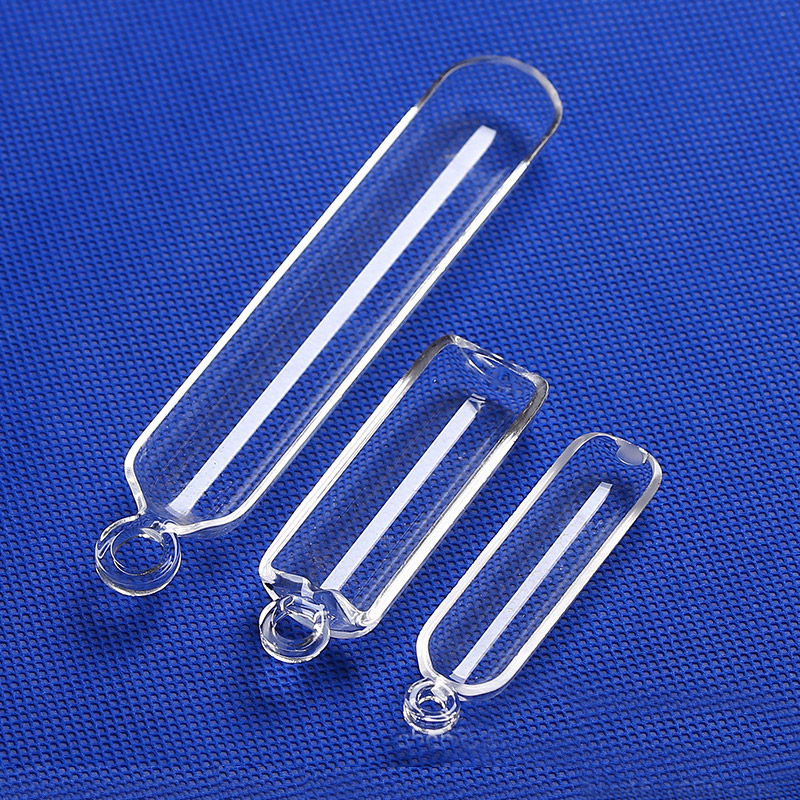
Custom Lab Fused Quartz Boat
Precision-welded 99.98% SiO₂ combustion boat for calcination, metallurgical testing, and laboratory chemical vapor reactions with exceptional chemical inertness.
View Specifications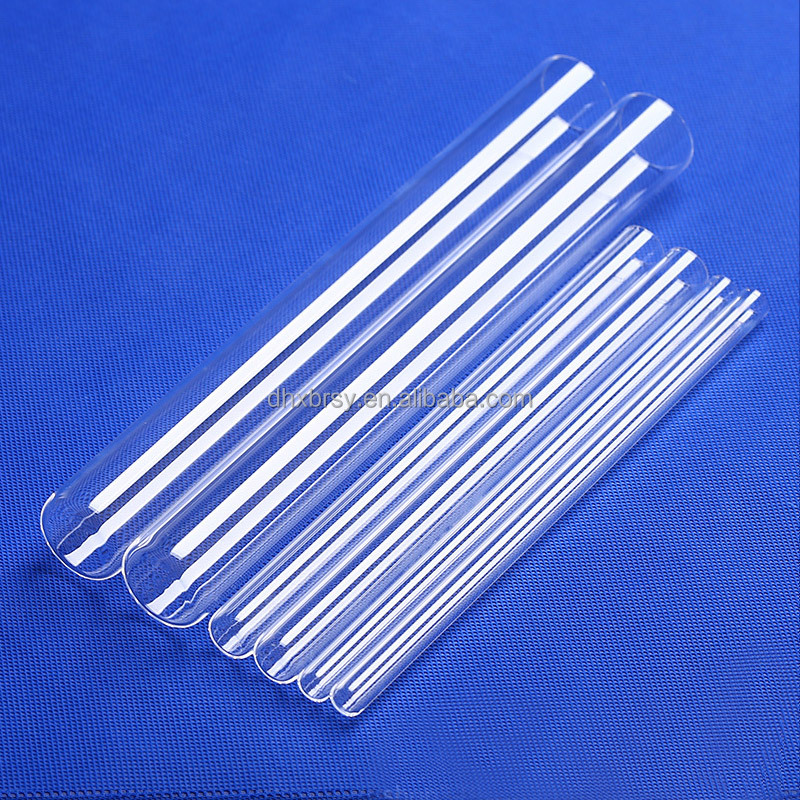
One-End Closed Quartz Laser Tube
Heavy-duty translucent fused silica tube with sealed spherical or flat end, rated for up to 1400°C short-term exposure in industrial laser machinery.
View Specifications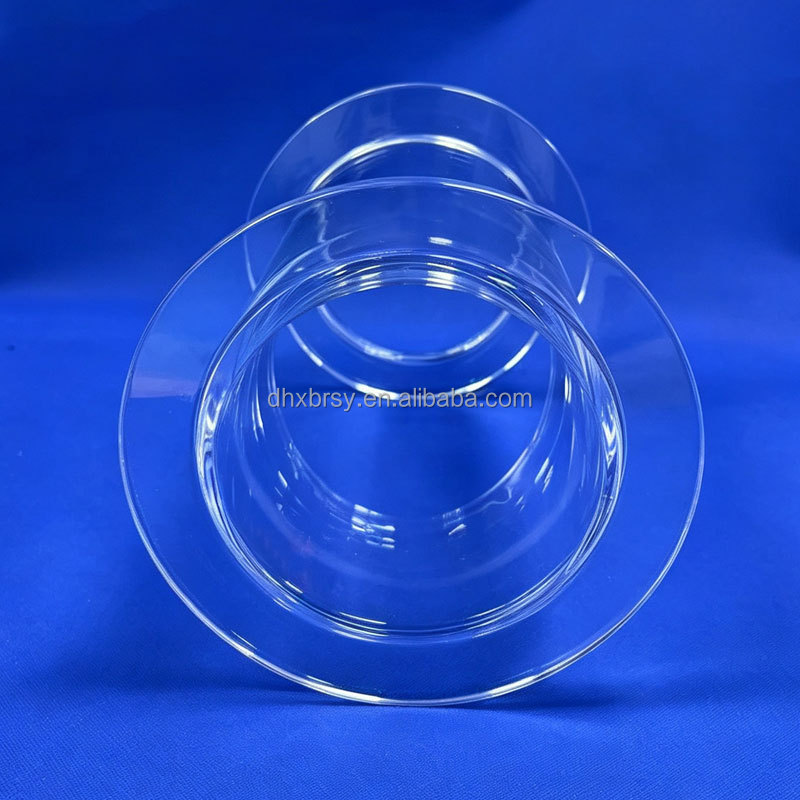
Double Flange Quartz CVD Cylinder
Transparent fused silica process cylinder with precision-ground double flanges for high-vacuum sealing in semiconductor and chemical deposition furnaces.
View Specifications
Ultra-Thin Laser Quartz Sheet
Optically flat fused quartz wafers (0.1mm–0.5mm) with 99.99% SiO₂ content for beam splitters, laser protection windows, and precision optical sensors.
View Specifications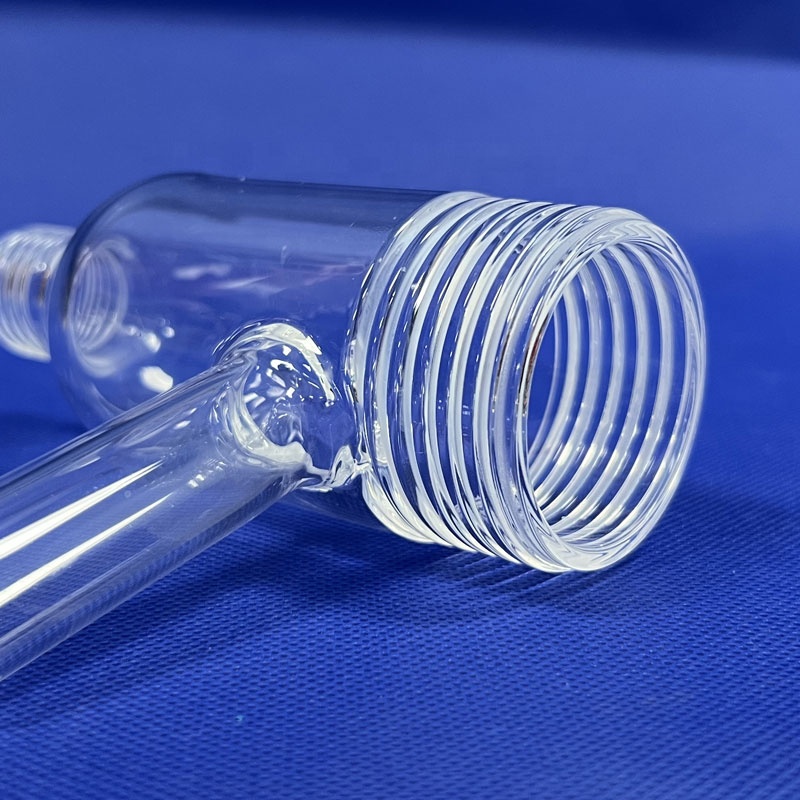
Threaded Quartz Reaction Tube
Integrated side-arm quartz vessel featuring precision threaded ports for inert gas purge, photochemical synthesis, and specialized laser fluid cooling loops.
View Specifications
Quartz Capillary Laser Flow Tube
Precision bore annealed capillary tube rated for 1200°C continuous service, tailored for lamp cooling jackets, laser diode conduits, and fluidic guidance.
View SpecificationsExecutive Summary: The Role of Quartz Flow Tubes in Industrial Laser Infrastructure
In high-power solid-state laser architectures, flashlamp-pumped systems, and industrial diode arrays, the laser flow tube serves as an indispensable thermo-optical envelope. Functioning simultaneously as a coolant channel and an optical radiation conduit, the flow tube isolates pump lamps and laser active elements (such as Nd:YAG, Alexandrite, or Er:YAG rods) while channeling deionized water or specialized refrigerants at velocity rates exceeding 5 to 15 liters per minute. The operational integrity of the entire resonator hinges on the quartz glass's optical transmission, hydrodynamic resistance, and ability to survive rapid pulsed thermal cyclings without micro-fracturing.
Dnipro (formerly Dnepropetrovsk), long recognized as the aerospace, defense, and heavy metallurgy epicenter of Ukraine, is currently experiencing a structural recalibration toward high-precision automated manufacturing, laser surface cladding, and military-grade optical maintenance. With local industrial enterprises—from missile engineering facilities to metallurgical plants along the Dnieper River—modernizing aging solid-state laser cutting tools and integrating advanced multi-bore laser flow tubes, sourcing reliable quartz components with certified chemical purity and geometric precision has become a critical procurement priority.
This industry whitepaper evaluates the top 10 international and regional manufacturers providing fused quartz laser flow tubes and specialized apparatus suitable for Dnipro's challenging operating environment, detailing optical physics parameters, material degradation factors, and strategic supply chain protocols.
Top 10 Quartz Laser Flow Tubes Manufacturers & Suppliers
An objective evaluation based on technical manufacturing capabilities, raw material purity, CNC geometric tolerance handling, and export logistics support for Ukrainian engineering contractors.
Lovri Quartz Products Co., Ltd.
- Origin: Lianyungang, Jiangsu, China (Primary Quartz Cluster).
- Core Competency: Complete vertical integration from raw silica ore pulverization and acid pickling to 4-axis CNC drilling, custom slotting, multi-bore drawing, and lathe sealing.
- Laser Tube Specialty: Triple-bore, double-bore, and C-shaped flow tubes; SAM doped (Cerium/Samarium) selective absorption sleeves; JGS1 UV synthetic fused silica.
- Quality Safeguards: 100% polarization stress testing post-annealing (1200°C), SGS onsite verification, and custom prototype runs starting from 1 unit.
- Dnipro Fit: Cost-to-performance leader with dedicated shock-proof air freight packaging for Dnipro delivery.
Heraeus Conamic (Germany)
- Core Competency: Global benchmark for ultra-pure synthetic fused silica (Suprasil®) and high-purity natural quartz (Spectrosil®).
- Laser Tube Specialty: Extreme UV damage resistance, zero bubble inclusions, ideal for excimer lasers and high-repetition pulsed flashlamp cavities.
- Market Consideration: Exceptional optical quality with high institutional prestige, though characterized by substantial cost premiums and lengthy lead times for custom drawings.
Momentive Technologies (USA)
- Core Competency: Pioneer in semiconductor-grade fused quartz tubing and high-temperature specialty materials.
- Laser Tube Specialty: High dimensional consistency tubing, low hydroxyl (OH) content tubing preventing thermal expansion anomalies during continuous laser firing.
- Market Consideration: Well-suited for heavy industrial setups in Dnipro's defense enterprises; requires large procurement batches.
Tosoh Quartz Corporation (Japan)
- Core Competency: Extreme precision fabrication for semiconductor CVD/etch jigs and ultra-clean optical tubes.
- Laser Tube Specialty: Sub-micron precision machining for laser flow cells, flow cytometers, and specialized cooling jackets with micro-fluidic channels.
- Market Consideration: Top-tier surface roughness (Ra < 0.5nm), primarily reserved for state research labs and advanced optics.
Saint-Gobain Quartz (France)
- Core Competency: Quartzel® wool and high-purity silica products for aerospace, military, and laser industrial furnaces.
- Laser Tube Specialty: High-temperature stability sleeves, reinforced quartz sight glasses, and heavy-wall discharge conduits.
- Market Consideration: Direct European logistics pathways, though standard catalog sizes dominate over rapid prototype flexibility.
QSIL SE (Germany)
- Core Competency: Specialized hollow fused silica glass cylinders and hollow fibers with doped profiles.
- Laser Tube Specialty: Samarium-doped glass laser flow tubes designed to filter 1064nm parasitic oscillations and absorb UV pump radiation, protecting the Nd:YAG crystalline rod.
- Market Consideration: Standard supplier for EU-manufactured laser machinery operating in Central/Eastern Europe.
Technical Glass Products (USA)
- Core Competency: Premier custom quartz fabrication, lathe turning, flame polishing, and scientific glassblowing.
- Laser Tube Specialty: Custom-bent dual-flow envelopes, flange-welded cooling sleeves, and bespoke medical laser flow assemblies.
- Market Consideration: Strong prototyping engineering capability with moderate lead times across international corridors.
Swift Glass Company (USA)
- Core Competency: CNC glass cutting, waterjet machining, edge beveling, and thermal tempering of optical quartz.
- Laser Tube Specialty: Protective flow tube outer envelopes, polished viewing ports, and flat multi-layer laser filter plates.
- Market Consideration: Ideal for flat-geometry optical shields and heavy-wall protective outer barriers.
National Scientific Quartz (UK)
- Core Competency: Specialized laboratory glassware, spectroscopic quartz flow cuvettes, and chromatography accessories.
- Laser Tube Specialty: Precision capillary flow tubes, mini-bore cooling conduits for diagnostic and low-power medical diode lasers.
- Market Consideration: High accuracy in micro-dimensions; primarily serves Dnipro's academic and diagnostic hospital centers.
Regional Ukrainian & Polish Quartz Workshops
- Core Competency: Secondary modification, flame re-sealing, torch welding, and emergency replacement fitting.
- Laser Tube Specialty: Rapid repair of damaged flanges, rebuilding broken lamp jackets, local retrofitting of foreign-made laser rigs.
- Market Consideration: Relies heavily on imported raw silica tubes (e.g., from Lianyungang/Lovri Quartz) for raw blank processing.
Material Engineering & Optical Performance Parameters
Comparative reference parameters for specifying fused quartz grades in high-stress laser cooling applications.
| Property Parameter | JGS1 (Synthetic Fused Silica) | JGS2 (Fused Natural Quartz) | JGS3 (Electrically Fused Quartz) | Samarium-Doped Quartz (10% Sm₂O₃) |
|---|---|---|---|---|
| Primary Silica Purity (SiO₂) | ≥ 99.999% | ≥ 99.99% | ≥ 99.98% | Silicate Matrix + Doping |
| Spectral Transmission Range | 185 nm – 2500 nm (Deep UV) | 220 nm – 2500 nm (Optical UV) | 260 nm – 3500 nm (Full IR) | Cut-off below 380 nm; peak absorption at 1064 nm |
| Hydroxyl (OH⁻) Content | High (>1200 ppm) or Low (<5 ppm) | Moderate (30 – 150 ppm) | Very Low (<10 ppm) | Process dependent (<50 ppm) |
| Thermal Expansion (20–300°C) | 5.5 × 10⁻⁷ /°C | 5.5 × 10⁻⁷ /°C | 5.4 × 10⁻⁷ /°C | ≈ 6.2 × 10⁻⁷ /°C |
| Solarization Resistance | Immune to UV Darkening | Moderate (prone after 1000h UV) | Prone under UV lamp discharge | Engineered UV Block |
| Typical Laser Cavity Use | Excimer lasers, 266/355nm Harmonics | Standard flashlamp cooling tubes | IR solid-state heater jackets | Nd:YAG, Alexandrite, Medical Laser Sleeves |
Critical Failure Analysis: Solarization & Cooling Fluid Dynamics
In high-repetition-rate laser systems operating in heavy industrial settings like Dnipro, laser flow tubes endure combined thermal, radiative, and hydraulic strains. Two primary mechanisms dictate premature tube decommissioning:
1. Solarization and Color Center Formation: High-power flashlamps emit substantial broad-spectrum UV energy below 250 nm. When ordinary quartz or low-grade fused silica is exposed to this flux, intrinsic trace impurities (such as Fe, Al, and Ti at parts-per-million levels) trap free electrons, creating color centers (E' centers). This manifests as a brownish discoloration of the tube walls. As transmission drops, the tube absorbs the pump light instead of transmitting it to the laser crystal, resulting in rapid output power decay and intense thermal stress along the inner wall.
2. Micro-Cavitation & Flow Induced Resonances: Coolant velocity in high-power Nd:YAG or Alexandrite cavities often approaches turbulent thresholds (Reynolds numbers > 4,000). If the inner surface of the flow tube exhibits micro-striations from inferior drawing dies, or if eccentricity exceeds 5%, localized cavitation pockets emerge. The collapsing micro-bubbles cause pitting along the quartz surface, degrading beam wavefront uniformity and ultimately seeding catastrophic hoop stress fractures.
Localized Applications Across the Dnipro Industrial Matrix
How specialized quartz tubes empower Dnipro's strategic manufacturing, aerospace rebuilding, and heavy metallurgical infrastructure.
Aerospace & Defense Rocketry Maintenance
Dnipro hosts world-renowned aerospace design bureaus and machine-building plants (including facilities historically connected to Pivdenmash). Precision double-bore and triple-bore quartz flow tubes are deployed in flashlamp-pumped solid-state lasers utilized for micro-drilling turbine cooling channels, dynamic balancing of missile propulsion parts, and high-energy laser rangefinding calibration.
Heavy Metallurgy & Pipe Laser Cladding
Along Dnipro's metallurgy belt, intense wear on pipe-rolling mandrels, continuous casting guides, and mining machinery demands heavy-duty laser cladding. Multi-kilowatt direct-diode and Nd:YAG laser cladding heads utilize heavy-wall transparent fused silica sleeves to isolate water-cooled optics from explosive slag spatter, high heat, and molten metal splashes.
Modernization of Machine Tool Laser Cutters
Hundreds of fabrication workshops in the Dnipropetrovsk Oblast rely on ruggedized laser cutting and welding systems. Replacing degraded OEM flow tubes with precision-annealed quartz sleeves prevents optical distortions in the cavity, restoring beam quality (M² factor) and stabilizing power output across long cutting shifts in structural steel processing.
Medical & Aesthetic Laser Service Centers
Dnipro's private medical and dermatological clinics operate advanced Alexandrite (755nm) and Nd:YAG (1064nm/532nm) aesthetic lasers. Samarium-doped (Sm₂O₃) flow tubes are essential consumable parts that filter dangerous parasitic laser frequencies and absorb stray UV, ensuring patient safety and lengthening the lifespan of costly laser rods.
Strategic Trends in the Dnipro Industrial Laser Procurement Market
The operating landscape for Dnipropetrovsk industrial equipment buyers has experienced structural realignments over the past 36 months. Procurement directors, university researchers, and shop floor managers face unique supply chain pressures that dictate new sourcing habits:
1. Decoupling from Unreliable Regional Intermediaries: Historically, many Dnipro enterprises procured quartz apparatus through regional distributors with multiple markups. Geopolitical dislocations and supply shocks have prompted engineering departments to establish direct manufacturer-to-client pipelines with primary quartz processing hubs like Lianyungang, China, securing stable batch traceabilities and OEM custom drawing adaptations.
2. Rise of Re-Engineering & Custom Dimension Adaptation: Much of the industrial laser equipment in central Ukraine represents a blend of European, American, Japanese, and domestic machines. Finding off-the-shelf catalog flow tubes for legacy 10kW laser cutters or retrofitted defense systems is often impossible. Procurement now prioritizes suppliers capable of receiving CAD drawings (DWG, STEP, PDF) and delivering low-volume custom prototypes (1–5 pieces) within compressed timeframes.
3. Stricter Demands for Certification & Annealing Verification: With operational budgets constrained, premature component failure carries an intolerable downtime cost. Procurement contracts across Dnipro increasingly mandate SGS factory assessment verification, RoHS material compliance certificates, and polarization stress test reports to guarantee that internal stress birefringence won't shatter the flow tube under the thermal shock of rapid laser firing.
Why Dnipro Buyers Partner with Lovri Quartz
Built upon the world's most concentrated silica refining base, Lovri Quartz delivers high-precision laser flow tubes and specialized apparatus directly from our factory floor.
14,271 m² In-House Production Hub
Assessed and verified onsite by SGS Group. We control every stage of manufacturing: raw quartz lump sizing, crushing, acid pickling to 99.99% SiO₂, tube drawing, rotary lathe welding, and cleanroom packaging.
Precision CNC Laser Tube Machining
Equipped with specialized 4-axis diamond tooling CNC machining centers capable of precision-drilling fluid ports, slotting, milling flat reference surfaces, and generating tight concentric multi-bore channels (±0.05 mm tolerance).
Certified Polarization Stress Inspection
Every single flow tube batch undergo high-temperature annealing at 1200°C followed by controlled cooling to relieve internal thermal stresses, verified on transmission polariscopes to eliminate cracking hazards.
Full Customization from Drawing (MOQ: 1 Pc)
Whether you require single replacement tubes for an obsolete laser system or volume batches of multi-bore flow cells for series production, we accept STEP, DWG, and PDF files with rapid engineering feasibility reviews.
Specialized Shock-Proof Air Packaging
We deploy triple-cushion custom molded EPE foam, heavy-wall reinforced cartons, and ISPM-15 export wooden crates specifically designed to ensure zero breakage during multimodal transit into the Dnipro region.
Lianyungang Cluster Price Advantage
Located at the epicentre of China's quartz refining industry, we source natural silica raw material and gas fuels at source costs, passing significant cost savings directly to European end-users without intermediary markups.
Frequently Asked Questions for Dnipro Buyers
Detailed technical, logistics, and quality assurance solutions to address common purchasing challenges in the Dnipro area.
How do I select between JGS1 synthetic silica, JGS2 natural quartz, and Samarium-doped quartz for a laser flow tube?
The choice depends strictly on your laser active medium and pumping mechanism. For UV harmonic lasers (266 nm or 355 nm) or excimer cavities, JGS1 is mandatory due to its near-zero metallic impurity profile and superior UV transmission without solarization. For conventional industrial Nd:YAG flashlamp pumping, JGS2 provides an optimal balance between optical efficiency and cost. If your application involves high-energy Nd:YAG or Alexandrite medical systems where 1064 nm parasitic laser emission causes crystal depopulation, or where unabsorbed UV radiation damages the crystal rod, choose Samarium-doped quartz (typically 10% Sm₂O₃), which filters out wavelengths below 380 nm and selectively absorbs at 1064 nm while passing pump wavelengths.
What dimensional tolerances can you maintain for multi-bore and C-shaped quartz flow tubes?
For standard round single-bore tubes, our continuous draw lines maintain outer diameter (OD) and inner diameter (ID) tolerances within ±0.05 mm to ±0.1 mm, with wall concentricity better than 95%. For precision CNC-machined components, custom-drilled multi-bore flow tubes, and C-shaped cavities, our CNC grinding and diamond polishing centers achieve bore-to-bore spacing tolerances of ±0.03 mm and surface finishes down to Ra < 0.2 µm. Such tolerances are crucial in Dnipro's high-flow cavities to prevent flow vortices and localized hot spots.
How is fragile quartz glass shipped to Dnipro without breakage under current logistics conditions?
Our packaging protocols are engineered specifically for export to European and Ukrainian destinations. Each quartz flow tube is thoroughly cleaned, degreased, and sealed in an anti-static dust-free polyethylene sleeve. It is then encased in form-fitting, high-density expanded polyethylene (EPE) foam cushioning with individual chamber cutouts. The foam core is placed within a double-wall corrugated carton, which is subsequently packed into a heavy-duty plywood crate lined with secondary shock dampeners. Shipments to Dnipro are routinely routed via European air freight hubs (e.g., Warsaw, Katowice, or Vienna) and delivered via overland express freight (Nova Poshta, Meest, or DHL) directly to your facility gate.
Can Lovri Quartz manufacture replacement flow tubes from a broken sample or legacy engineering drawing?
Yes. Many legacy laser cutters, metallurgical welding cavities, and research laser systems in Dnipro lack original manufacturer support. You can provide a CAD file (STEP, DWG, DXF) or a detailed dimensioned sketch with callouts for outer diameter, inner bore diameter, total length, fluid port angles, and flange details. If only a damaged physical piece remains, our engineering team can work from your calibrated caliper measurements and high-resolution photographs to reconstruct precise shop fabrication drawings.
What documentation and quality certifications accompany your shipments?
Each delivery includes a comprehensive documentation pack: Material Certificate of Conformance (verifying ≥99.99% SiO₂ content and trace metal limits), Dimensional Inspection Data Sheet with recorded micrometric measurements, RoHS 2.0 Compliance Certification, and upon request, UV-Vis-NIR Spectrophotometer Transmission Curves and Polarization Stress Inspection Certificates. Our manufacturing operations comply with ISO 9001 management protocols and hold SGS onsite factory assessment accreditation.